M14 Drive
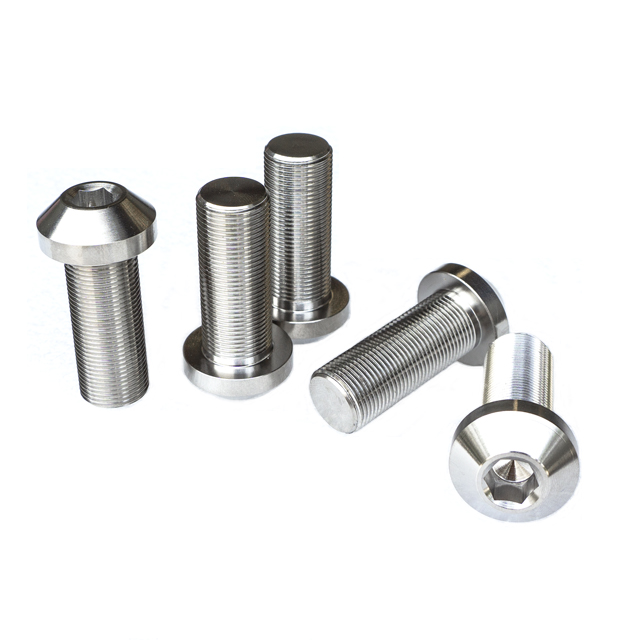
Manufactured from aerospace-certified Baoji Grade 5 (Ti-6Al-4V) titanium bars. Every sprocket fastening bolt incorporates precision rolled threading, high shear fracture tolerances, and specialized surface passivations designed for cyclical fatigue environments.
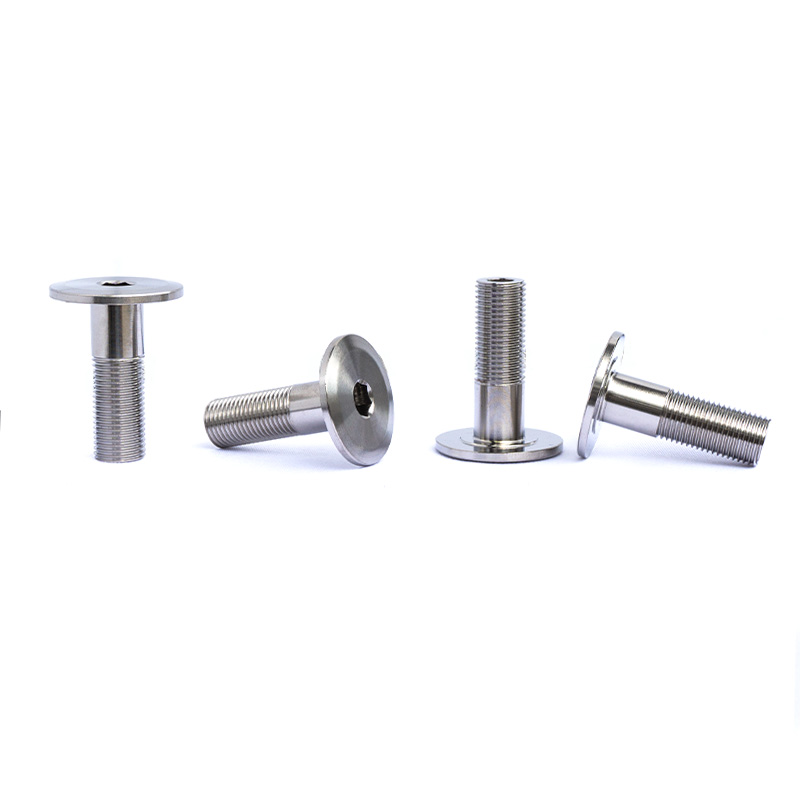
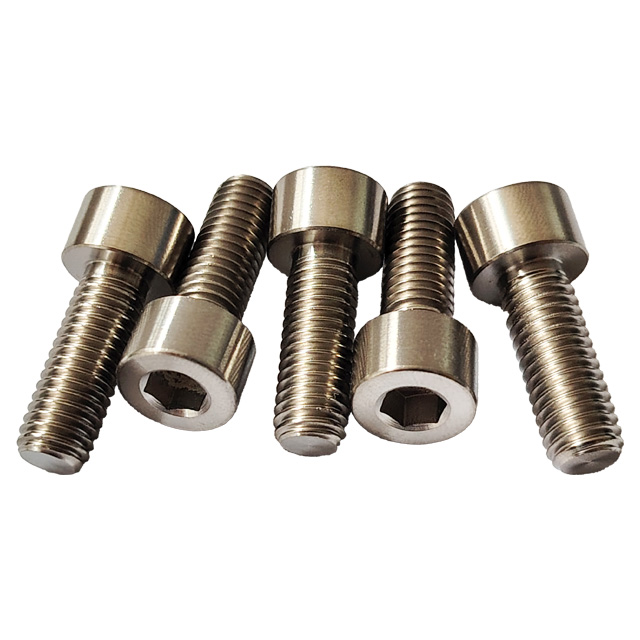
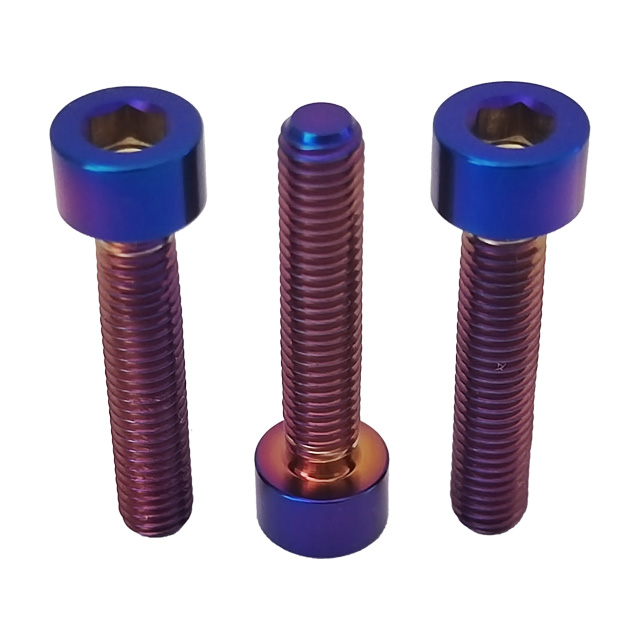
In dynamic mechanical drives, sprocket bolts operate under severe tension-shear multi-axial fatigue states. Understanding the fundamental material mechanics between Ti-6Al-4V Grade 5 and legacy Grade 10.9 steel prevents fatal catastrophic drive-hub sheared bolts.
The primary point of fatigue nucleation on mechanical sprockets occurs at the first engaged root thread under the fastener head flange. Traditional low-cost machining cuts through the titanium grain microstructure, leaving micro-notches that drastically accelerate cyclic shear cracking under shock loading. Navzo exclusively implements cold-work thread rolling post-solution annealing.
Thread rolling creates continuous compressive residual stress fields across thread roots. This grain rearrangement increases continuous shear load endurance limits by upwards of 34% compared to turned screws, critical for high-torque mechanical agricultural drivetrains and motorsport countershaft hubs operating across Mogilev's demanding cold-weather cyclic duty runs.
Titanium possesses an affinity for spontaneous formation of protective TiO₂ passive films, providing unmatched resistance to chloride and chemical attack. However, bare titanium sliding against steel or alloy hubs can exhibit adhesive wear, known in mechanical engineering as galling. For industrial sprocket hubs, unaddressed micro-fretting leads to loosened clamping torques.
Navzo eliminates thread seizure through rigorous tribological controls: Physical Vapor Deposition (PVD) titanium carbo-nitride hard films and controlled anodic oxidation. Furthermore, we mandate anti-seize copper-moly pastes during torque-up to standardize friction coefficients (μ = 0.12 to 0.15), ensuring clamping preloads remain consistent through harsh operating shifts.
| Alloy Specification | Yield Strength (Rp0.2, MPa) | Tensile Strength (Rm, MPa) | Density (g/cm³) | Endurance Limit (10⁷ Cycles) | Corrosion & De-icing Resistance |
|---|---|---|---|---|---|
| Navzo Ti-6Al-4V Grade 5 (Cold Rolled) | 828 - 910 | 895 - 1020 | 4.43 | 510 MPa | Immune to road salts, urea, and industrial moisture |
| Structural High-Tensile Steel (Class 10.9) | 900 - 940 | 1000 - 1040 | 7.85 | 420 MPa | Poor; Rapid hydrogen embrittlement & rust |
| Austenitic Stainless Steel (A2-70 / 304) | 450 | 700 | 7.90 | 240 MPa | Moderate; Prone to stress corrosion cracking |
| Grade 2 Commercially Pure Titanium | 275 | 345 | 4.51 | 180 MPa | Excellent; Insufficient shear for dynamic drive hubs |
Mogilev serves as an industrial nucleus in Eastern Europe, characterized by heavy machinery manufacturing, chemical processing facilities, agricultural equipment works, and rigorous winter transport systems. Navzo titanium sprocket fasteners solve distinct regional operating challenges.
Mogilev agricultural machinery operates in moist podzolic soils saturated with nitrogen-potassium fertilizers. Steel sprocket hardware on feeder-house drives and grain elevators corrodes rapidly, inducing unseating. GR5 titanium bolts offer absolute chemical passivity combined with extreme dynamic tensile capacity.
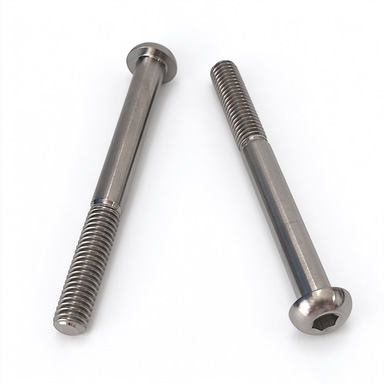
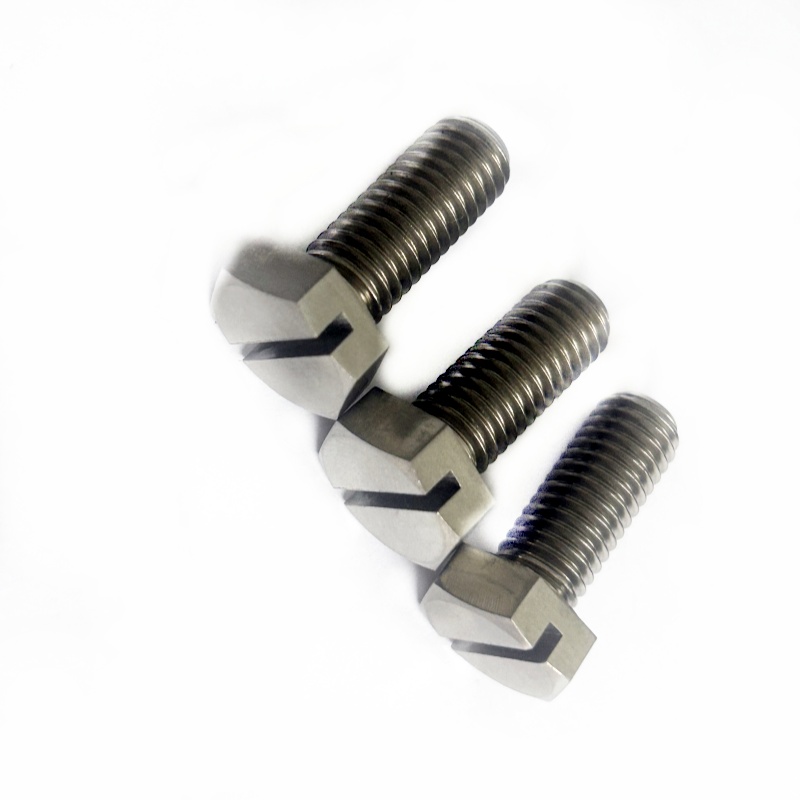
In local chemical, synthetic fiber, and bulk fertilizer processing plants, conveyor roller chains face aggressive sulfurous atmospheres. Navzo custom titanium slotted hex and umbrella head sprocket bolts resist pitting and chloride cracking, eliminating downtime during processing shifts.
Regional motorsport teams across Mogilev recognize that reducing rotational unsprung mass on rear hubs enhances rear suspension reactivity and acceleration out of corners. Our drilled hex flange and tapered socket bolts reduce wheel hub rotating inertia by 44% compared to OEM steel hardware.
Procurement managers in Mogilev are pivoting from reactive short-lifecycle part replacement toward Lifecycle Cost Assessment (LCA). With salt de-icing during sub-zero Belarusian winters accelerating galvanization breakdown on steel grade 8.8 and 10.9 bolts, titanium fastener integration is shifting from an exotic upgrade to an essential operational hedge against mechanical line shutdown and frequent thread retorquing.
Headquartered on Yucai Road in the High-tech Development Zone of Baoji, Navzo Precision Titanium operates at the epicentre of global titanium raw material metallurgy, eliminating intermediate distributor margins and guaranteeing unadulterated mill pedigree.
Every single titanium sprocket bolt lot is mapped directly back to 100% vacuum-arc remelted (VAR) sponge titanium ingots. We issue EN 10204 3.1 chemical composition and tensile mechanical mill certificates with every Mogilev dispatch.
Equipped with high-precision Swiss-type turning centers, multi-station cold heading machines, and precision flat-die thread rollers capable of holding concentricity tolerances down to ±0.005mm for high-speed dynamic drive sprockets.
In-house anodizing, thermal blue oxidation, micro-arc oxidation (MAO), and titanium carbonitride PVD coatings. We calibrate layer depth to avoid dimensional variance on tight clearance metric threads (ISO 6g tolerances).


Since established in 2011, Navzo Precision Titanium has supplied Tier-1 racing teams, machinery builders, and precision distributors worldwide. As an on-site verified manufacturer ranked in bolts manufacturing excellence, we guarantee engineering-level technical support.
Clear, direct answers regarding customs clearance, metallurgical suitability, galvanic isolation, and ordering specifications for buyers in the Mogilev market.
Yes. Ti-6Al-4V Grade 5 provides minimum ultimate tensile strength of 895 to 1000 MPa and yield strength exceeding 828 MPa, matching the practical clamping tension of Class 10.9 steel fasteners while cutting total unsprung assembly weight by ~44%. For high-vibration sprocket drives, the superior elasticity modulus of titanium (~114 GPa versus ~210 GPa for steel) allows the bolt to absorb cyclic drive train shocks without yielding.
When noble titanium contacts an aluminum wheel or drive hub in the presence of conductive moisture (such as road de-icing salts used around Mogilev in winter), the potential difference can promote galvanic degradation of the aluminum. We resolve this by applying PVD barrier coatings, fluoropolymer dry-film lubes, or supplying titanium fasteners with broad-flange umbrella designs and composite isolation washers to distribute boundary clamp loads safely.
For standard catalogue metric dimensions (M5, M6, M8, M10, M14 in standard pitches), our MOQ starts at 100 to 200 pieces. Custom CNC parts built to technical drawings or sample specimens (PDF, STEP, DWG) typically require a trial run of 50 to 100 pieces. Standard delivery through expedited air logistics to Belarus takes 7–12 business days, while volume sea-rail multimodal shipments take approximately 25–35 days.
Because titanium's friction coefficient differs slightly from dry phosphate-coated steel, bolts should always be torqued using a calibrated torque wrench and a titanium-compatible anti-seize paste. As a general engineering baseline, titanium threads require approximately 80% to 85% of standard steel torque values to achieve identical clamping preload without risking thread necking or drive-socket deformation.
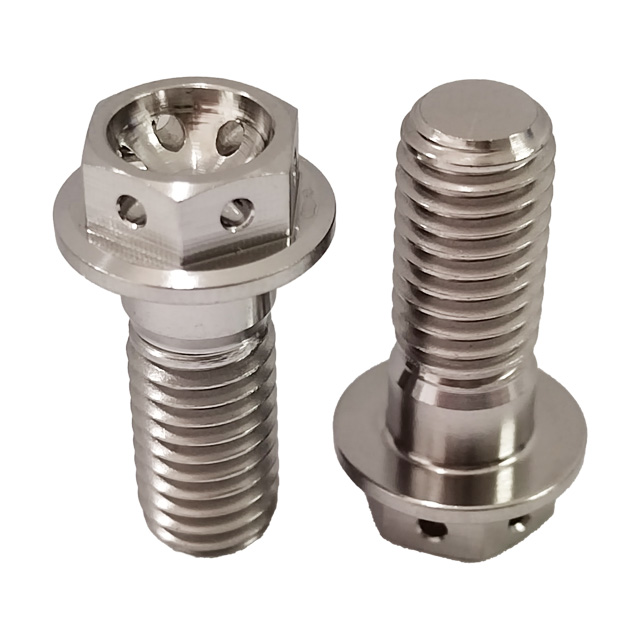
Yes. We manufacture hex flange bolts with pre-drilled cross-holes (standard 1.5mm to 2.0mm bore) across both the hex flats and the bolt shanks. This allows safety wire (lock-wire) or mechanical split-pinning to completely prevent bolt back-out under relentless operational vibration in combine harvesters, shaker tables, and racing motorcycles.
Every commercial consignment includes comprehensive quality paperwork: Mill Test Reports (MTR) demonstrating compliance with ASTM B348 / ASTM F136, optical dimensional measurement reports verifying ISO thread fits, and spectrographic analysis verifying trace elements (Fe ≤ 0.25%, O ≤ 0.20%, H ≤ 0.015%). Third-party SGS or TÜV verification can also be commissioned prior to dispatch.