Ti-6Al-4V
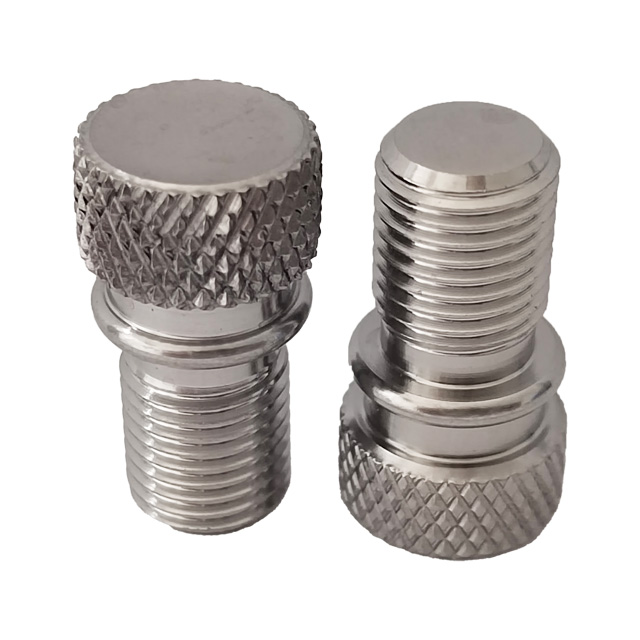
Manufactured strictly under ASTM B348, AMS 4928, and ISO 9001 standards from raw Baoji Titanium Valley ingot melts. Directly supplying Calgary machine shops, subsea completions, and downstream fabrication units.
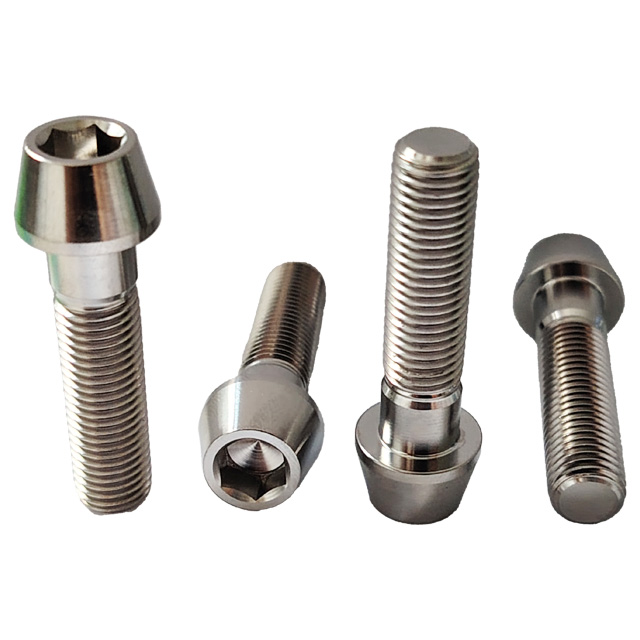
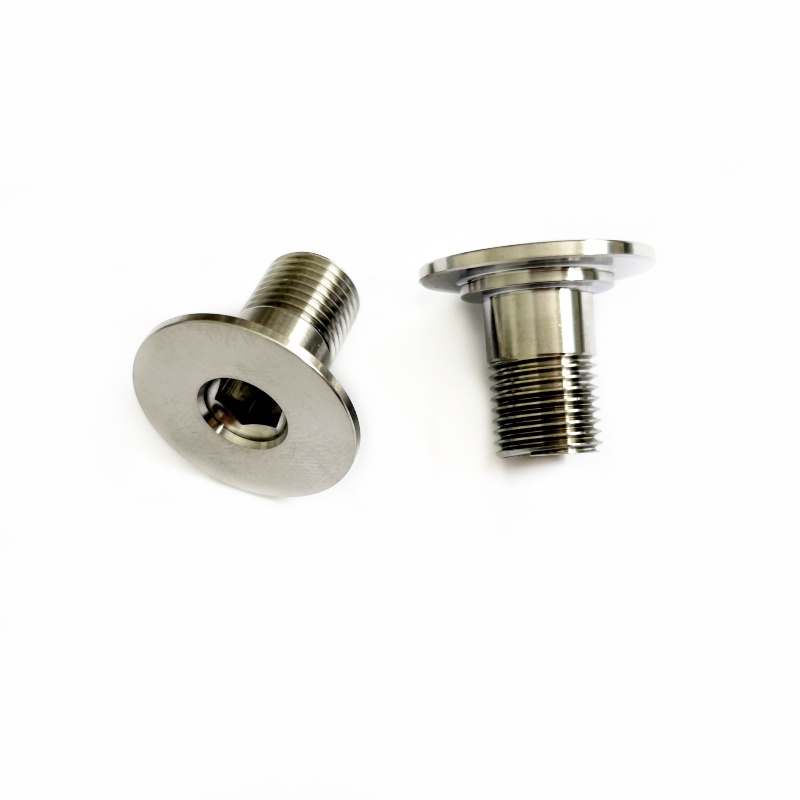
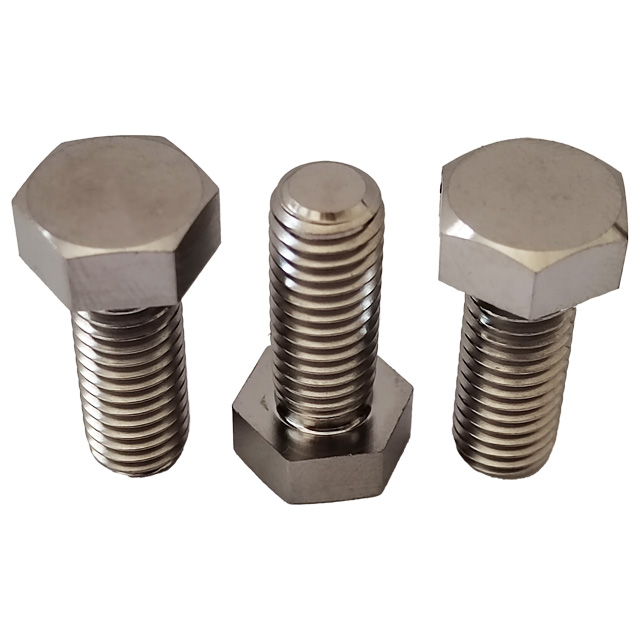
Calgary sits at the epicenter of Canada's heavy industrial, subsea valve manufacturing, pipeline engineering, and clean-tech innovation. Navzo delivers precision-machined titanium round, square, and hexagonal bars optimized for corrosive sour environments and sub-zero thermal stresses.
Directional drilling setups operating across the Western Canadian Sedimentary Basin (WCSB) require high-tensile, non-magnetic materials to eliminate electromagnetic interference on directional instrumentation. Navzo's GR5 (Ti-6Al-4V) rods guarantee zero magnetic permeability (< 1.00005) combined with yield strength surpassing 828 MPa, resisting downhole cyclical bending fatigue.
Processing wet sour hydrocarbons in the foothills and deep Alberta formations accelerates sulfide stress cracking (SSC) and chloride-induced pitting in typical 316SS and duplex steels. Our vacuum arc remelted (VAR) Grade 2, Grade 5, and Grade 7 (Palladium-alloyed) titanium rods comply with NACE MR0175 / ISO 15156, offering near-absolute immunity to pitting and crevice corrosion under low pH regimes.
Surface installations and oil transport infrastructure throughout Northern Alberta encounter extreme winter temperature drops. Standard martensitic alloys suffer steep ductile-to-brittle transitions. Navzo's Ti-6Al-4V ELI (Grade 23 / ASTM F136) ensures ultra-low interstitial oxygen content (<0.13%), ensuring reliable Charpy V-notch impact toughness and preventing shatter-rupture down to cryogenic levels.
Procurement criteria across Calgary engineering procurement construction (EPC) conglomerates are shifting from initial capital expenditure to whole-lifecycle integrity and decarbonization metrics.
Alberta's massive commitment to clean hydrogen corridors and Carbon Capture, Utilization, and Storage (CCUS) projects requires metals that resist supercritical CO2 acidic condensation and high-pressure hydrogen embrittlement. Navzo supplies specialized titanium billets and hex stock specifically chosen by Calgary engineering teams for high-integrity compressors, injectors, and monitoring manifolds.
Calgary precision machine shops face substantial labor and tool wear overheads when machining tough alloys. Navzo produces cold-drawn, peeled, and precision-centerless-ground titanium rods with h7 to h9 diametrical tolerances. Consistent microstructural grain size (ASTM Grade 5-8) reduces cutter chatter, lowers tool breakage, and cuts cycle times on multi-axis Swiss CNC turning centers.
Calgary procurement managers traditionally depended on multi-tier regional distributors, incurring heavy middleman markups and delayed lead times. Sourcing directly from Navzo's factory floor in Baoji provides raw mill pricing, rapid air cargo dispatch via Calgary International Airport (YYC), and integrated Pacific freight handling via the Port of Vancouver.
Evaluate exact physical, thermal, and mechanical parameters before drafting your procurement specifications.
| Alloy Specification | Nominal Chemistry | Density (g/cm³) | Yield Strength (Min MPa) | Charpy Impact @ -40°C | NACE MR0175 Compliance |
|---|---|---|---|---|---|
| Navzo GR5 (Ti-6Al-4V) | Ti-6Al-4V (Annealed) | 4.43 | 828 | ≥ 24 Joules | Fully Approved |
| Navzo GR5 ELI (Grade 23) | Ti-6Al-4V ELI (Low O2) | 4.43 | 795 | ≥ 34 Joules (Extreme Low Temp) | Fully Approved |
| Navzo Grade 2 CP Titanium | Unalloyed Titanium | 4.51 | 275 | High Ductility | Fully Approved |
| AISI 4140 Alloy Steel | Cr-Mo High Tensile Steel | 7.85 | 655 | Brittle Transition Risk | Requires Specific Tempering |
| 316L Stainless Steel | 16Cr-12Ni-2.5Mo | 8.00 | 220 | Moderate | Susceptible to Chloride Pitting |

Navzo Precision Titanium Products Co., Ltd. is situated in the High-tech Industrial Development Zone of Baoji, Shaanxi Province, China. Baoji produces over 60% of China's titanium sponge, ingots, and rolled raw materials. Being situated within this cluster shortens our supply pipeline, guarantees consistent chemical ingot control, and reduces processing costs.
Every titanium bar and fastener ships with comprehensive mill test certificates specifying chemical melt records, tensile/yield values, and ultrasonic non-destructive testing reports.
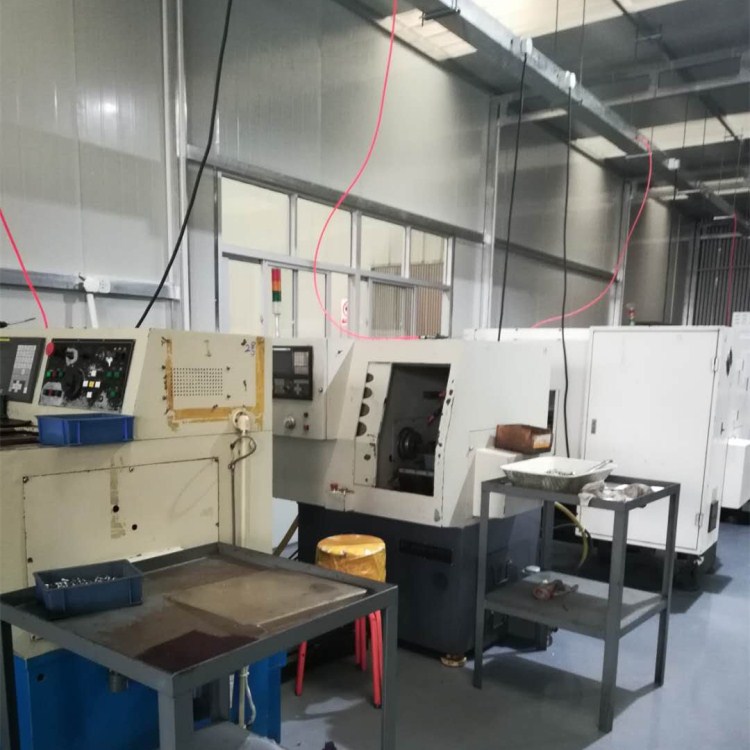
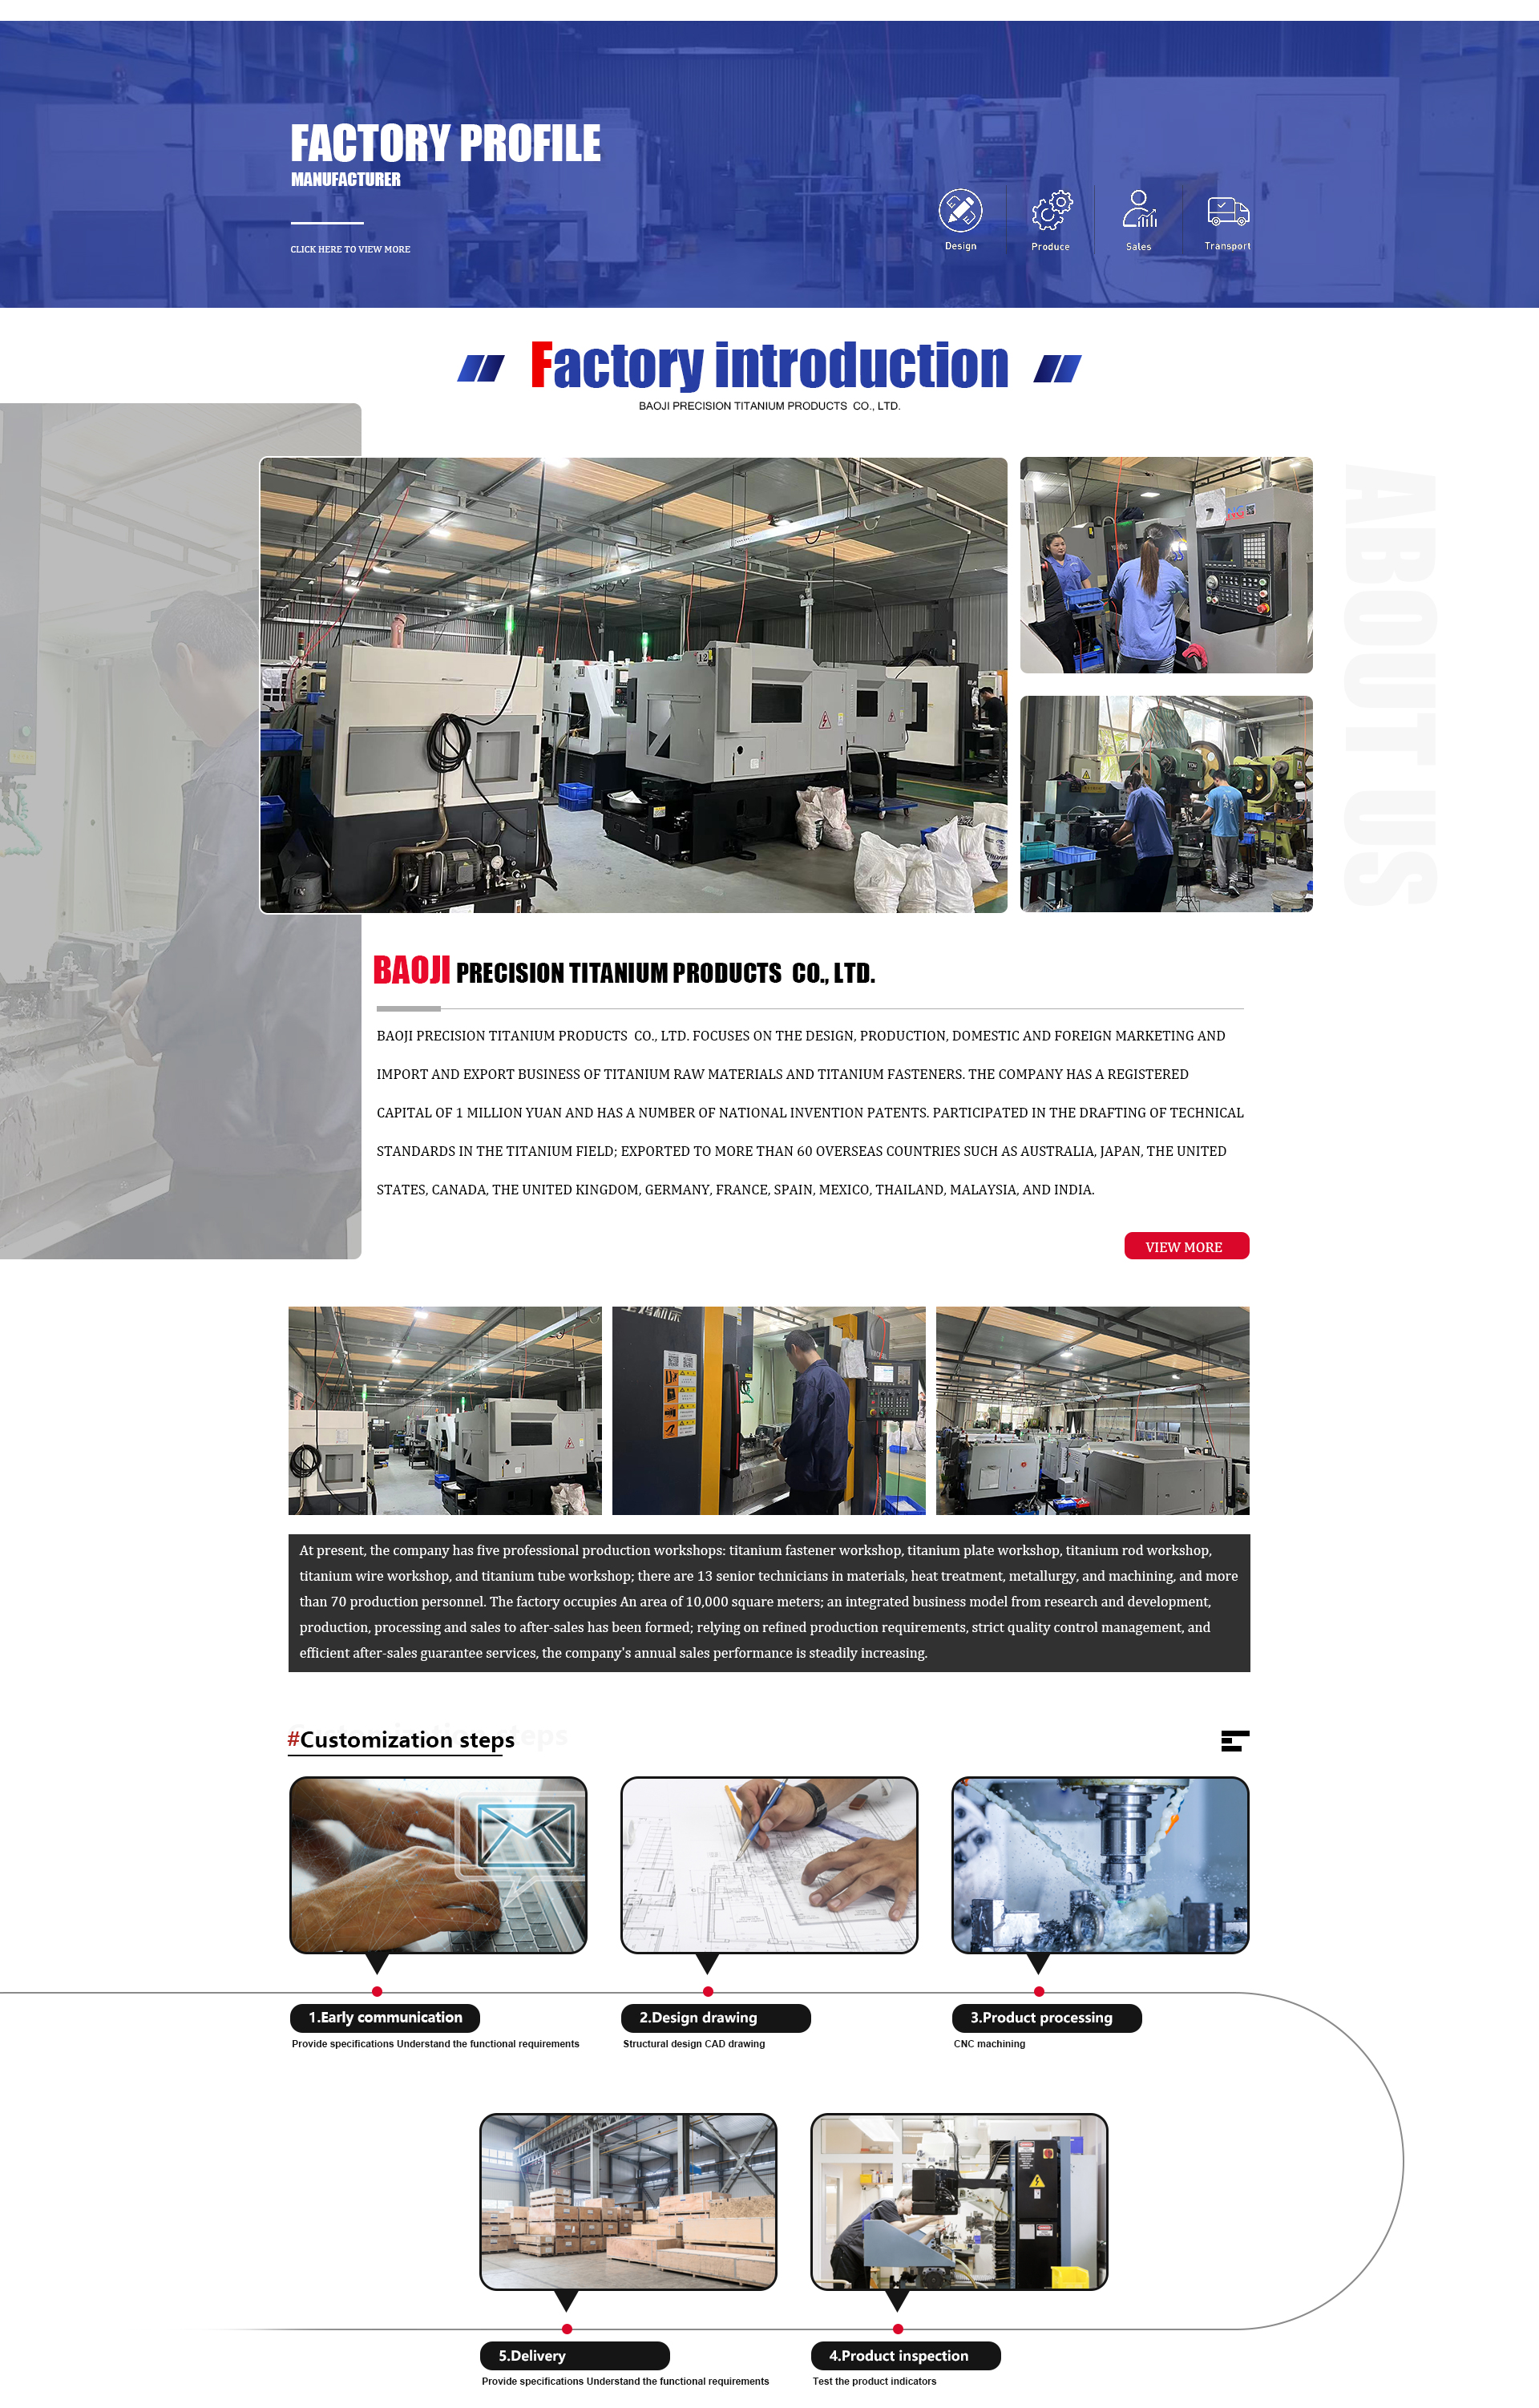
From centerless grinding lines down to micro-tolerance CNC turning, cold heading, and precision thread-rolling machines, our integrated workflow eliminates outsourcing delays.
Equipped with vacuum PVD coating, titanium micro-arc anodizing, sandblasting, and chemical etching stations to meet exact industrial and wear-resistant demands.
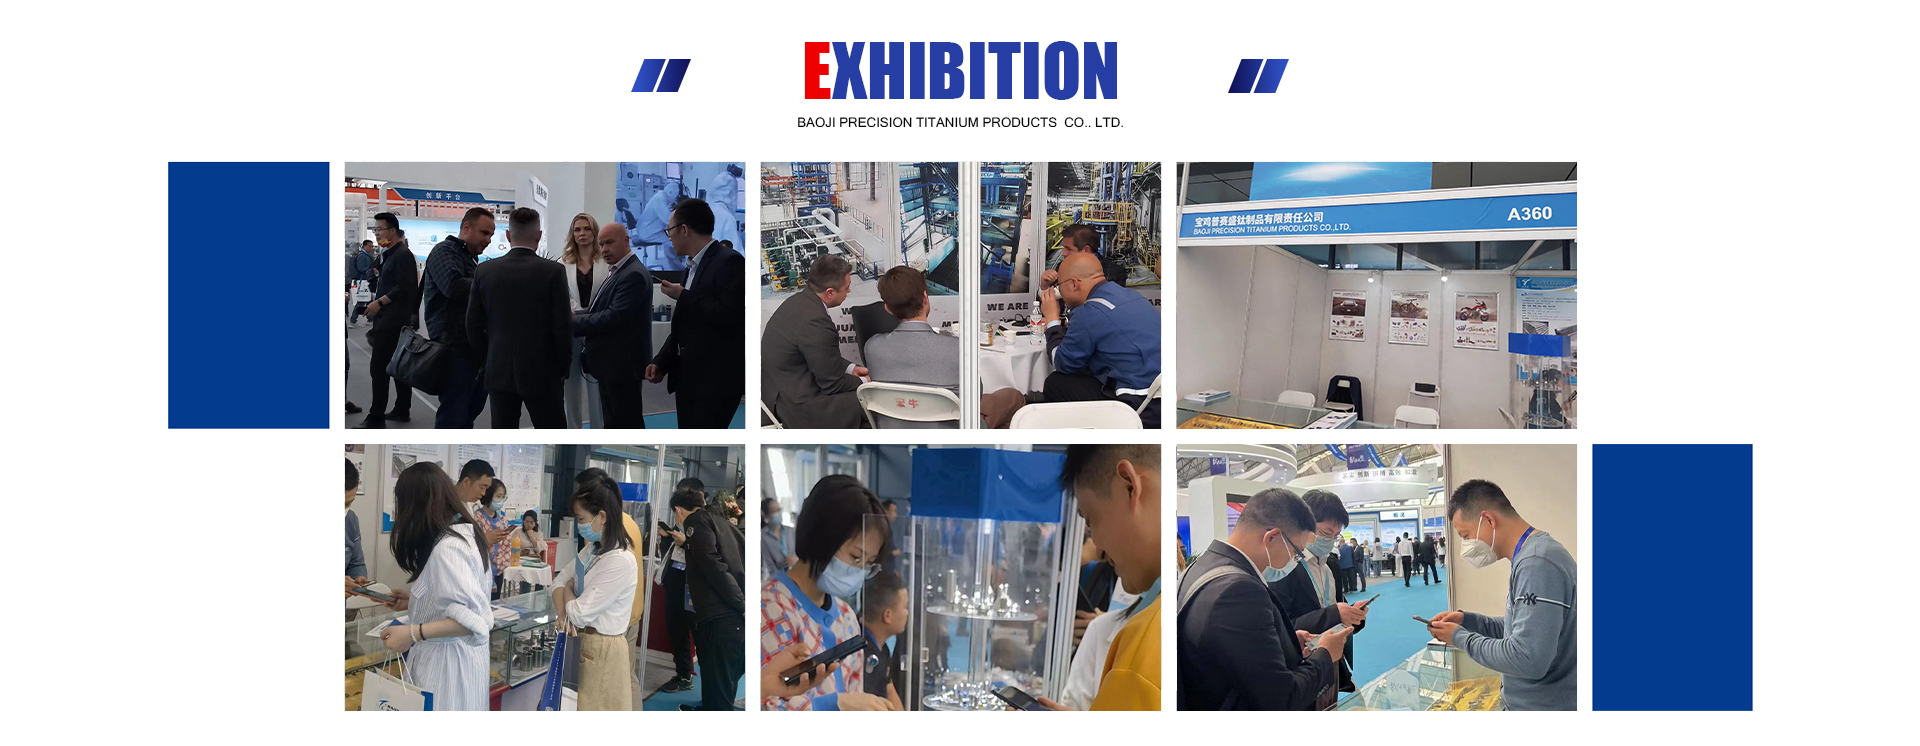
A closer look inside our machining, forging, and quality inspection workflows.
Clear, direct answers regarding customs, logistics, certifications, and technical machining questions.
For catalog sizes and standard mill bar orders, materials dispatch within 3–5 working days. Air express shipments (via DHL, FedEx, or air charter to Calgary YYC) average 5 to 8 business days transit time. Full container loads (FCL/LCL) routed via ocean freight to Vancouver followed by CP/CN rail transfer into Calgary logistics hubs average 18 to 25 days door-to-door.
We provide full commercial invoices, packing lists with correct HS codes (e.g., 8108.90 for wrought titanium bars and rods; 7318.15 for specialized fasteners), Certificate of Origin, and complete mill test certificates to ensure swift handling via your designated Canadian customs broker.
Yes. Our raw rods and hex bars are produced and certified to ASTM B348 (Standard Specification for Titanium and Titanium Alloy Bars and Billets), AMS 4928 (Aerospace Material Specification), and ASTM F136 (ELI Grade for critical surgical and downhole instruments). Ultrasonic testing to AMS 2631 Class A/AA is available on request.
Titanium threads are prone to adhesive galling under dry torquing. We recommend molybdenum disulfide (MoS2) anti-seize paste, nickel-based compounds, or our factory vacuum PVD and specialized surface conversion coatings. Our rolled threading technique compresses surface grain structure, yielding 30% higher wear life over cut threads.
For sizes currently in mill inventory, MOQs start as low as 10 to 25 kg to support prototyping and machine trials. For custom alloy remelting or non-standard hot extrusion sizes, MOQ ranges between 100 kg and 300 kg depending on target dimensions.
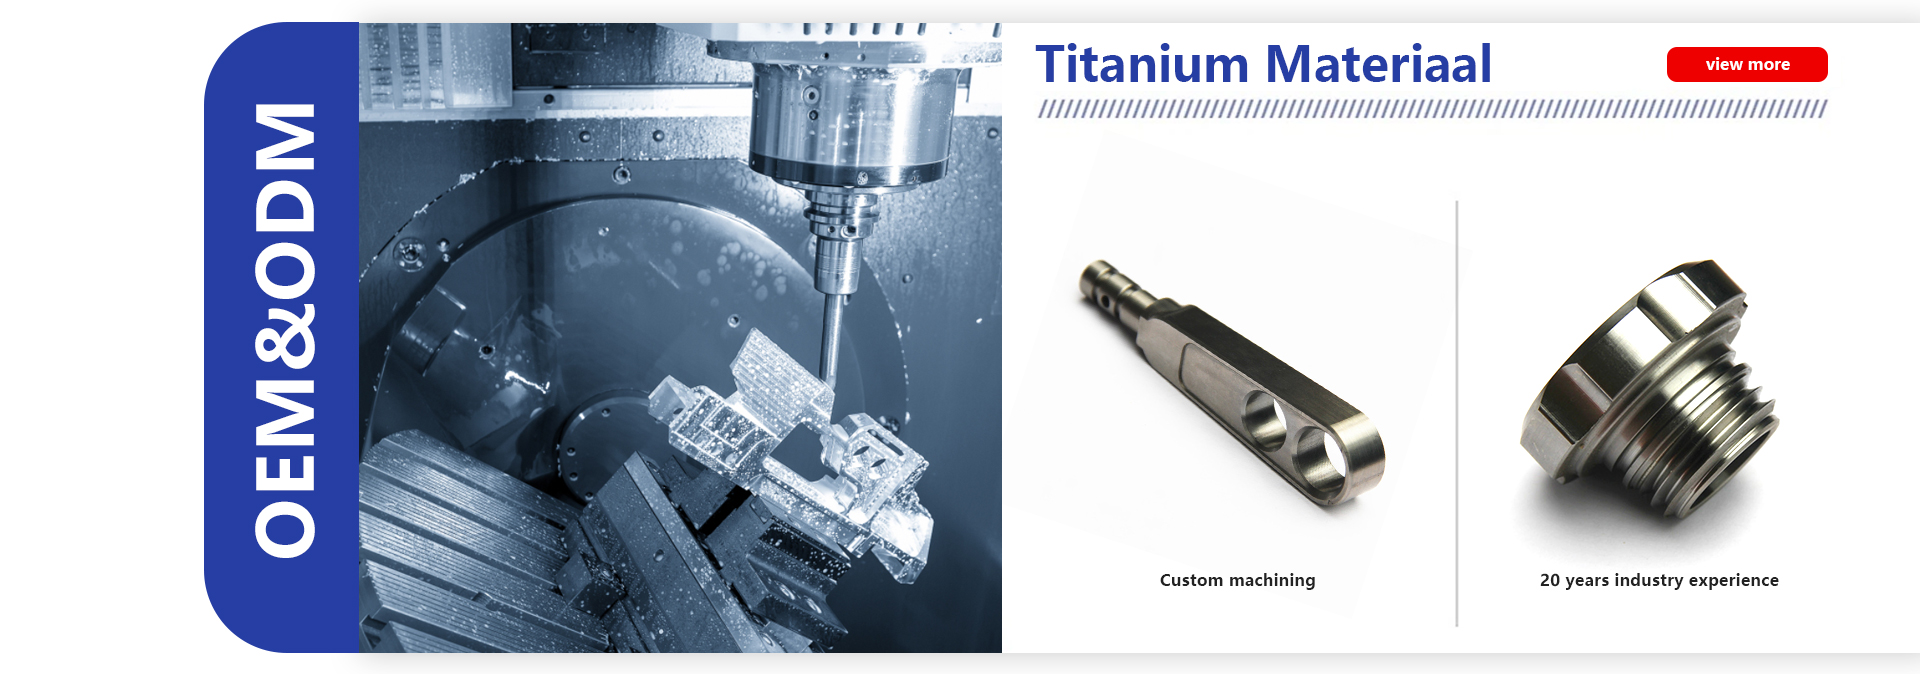
Yes. Our in-house engineering facility accepts 2D/3D models (STEP, IGES, DWG, PDF). Our engineers carry out design for manufacturability (DFM) reviews, evaluate tight geometric tolerances (GD&T), and program multi-axis CNC turn-mill stations to deliver completed parts right out of the box.
Whether you require standard ASTM B348 GR5 round bars, precision ground rods, or custom CNC machined oilfield fasteners, our bilingual technical engineering team is on standby. Submit your specs, BOM lists, or CAD drawings today for a rapid, transparent quotation within one business hour.