High-Performance Titanium Hardware & Anode Assemblies
Manufactured in Baoji, China utilizing ASTM B348 and ASTM B265 Grade 5 (Ti-6Al-4V) and Grade 1/2 commercially pure substrates. Engineered for harsh electrochemical baths, high-vibration automotive exhaust systems, and marine cathodic installations.
Top China Titanium Mesh Anode Exporter: Electrochemical Authority
Understanding the physics, metallurgy, and catalytic lifespan of Dimensionally Stable Anodes (DSA®) fabricated in China's metallurgical epicenter: Baoji, Shaanxi.
The Strategic Advantage of Chinese Titanium Valley Supply Chains
As the international transition toward green hydrogen, chlor-alkali optimization, copper foil electrodeposition, and impressed current cathodic protection (ICCP) accelerates, global engineering firms rely on a proven China titanium mesh anode exporter to supply dimensionally stable anodes capable of surviving extreme anodic polarization. China manufactures over 65% of global titanium sponge and processed mill products, with the epicenter located directly in Baoji, Shaanxi.
Navzo leverages this integrated raw material corridor. By sourcing pure ASTM B265 Grade 1 and Grade 2 titanium ingots directly from neighboring vacuum arc remelting (VAR) facilities, our chemical purity remains uncompromised with interstitial elements strictly controlled (Fe < 0.08%, C < 0.02%, N < 0.015%, O < 0.12%, H < 0.008%). This precise chemical threshold eliminates localized grain-boundary pit corrosion under intense electrocatalytic conditions.
When selecting a qualified titanium mesh anode exporter, foreign procurement managers must look beyond surface square meterage. Expanded titanium mesh requires precision micro-slitting and diamond mesh stretching that maintains uniform strand cross-sections without micro-fissures. Our automated expanding equipment ensures predictable current distribution profiles, critical for eliminating uneven noble metal coating depletion in electrochemical cell stacks.
Expanded Diamond Geometry
Standard expanded titanium mesh configurations utilize Long Way of Diamond (LWD: 2.5mm to 12.5mm) and Short Way of Diamond (SWD: 1.5mm to 6.0mm). This geometric arrangement provides high open-area ratios (> 45%) which promote rapid electrolytic gas evolution detachment (both $Cl_2$ and $O_2$), mitigating localized electrical resistance and hyper-polarization hotspots.
Multi-Stage Thermal Pyrolysis
Catalytic MMO (Mixed Metal Oxide) coatings are not applied via simple electroplating. Navzo utilizes up to 28 sequential automated coating-and-baking cycles (thermal decomposition at 450°C–520°C). This produces an interdiffused nanocrystalline solid-solution oxide structure ($IrO_2-Ta_2O_5$ or $RuO_2-TiO_2$) that anchors tenaciously into etched titanium crystal facets ($Ra \ge 3.5\,\mu m$).
Accelerated Life Standard (NACE)
Navzo anodes undergo Accelerated Life Testing in compliance with NACE TM0108 and ISO 15711. Tested in high-concentration $1.0\,M\ \text{H}_2\text{SO}_4$ electrolytes under ultra-high current densities of $10,000\text{ to }20,000\,\text{A/m}^2$, our anodes demonstrate endurance exceeding 120–350 continuous test hours, translating to a field working life of 5 to 15 years depending on bath parameters.
Catalytic Coating Formulations & Selection Guide
Selecting the correct MMO formulation dictates operational power consumption, bath longevity, and chemical resistance. Review our primary industrial catalytic series.
| Coating Formulation | Primary Reaction | Noble Metal Load ($g/m^2$) | Working Current Density | Key Industry Sectors |
|---|---|---|---|---|
| Ruthenium-Iridium-Titanium ($RuO_2-IrO_2-TiO_2$) | Chlorine Evolution Reaction (CER) | 8.0 – 25.0 g/m² | < 3,000 A/m² | Chlor-Alkali, Sodium Hypochlorite, Seawater Electrolysis, Ballast Water Treatment |
| Iridium-Tantalum Oxide ($IrO_2-Ta_2O_5$) | Oxygen Evolution Reaction (OER) | 12.0 – 40.0 g/m² | < 15,000 A/m² | Electrolytic Copper Foil, PCB Plating, Organic Wastewater Treatment, Acid Electroplating |
| Platinum Coated ($Pt-Ti$) | Hybrid Catalytic Anodic Protection | 1.5 – 5.0 µm Thickness | < 5,000 A/m² | Electroplating Gold/Rhodium, Hydrogen Production, Cathodic Impressed Current (ICCP) |
| Lead Dioxide ($Ti/\beta-PbO_2$) | High Overpotential Oxygen Evolution | 0.5 – 2.0 mm Layer | < 8,000 A/m² | Hydrometallurgy (Zinc/Copper Electrowinning), Phenolic Wastewater Destruction |
| Mixed Ternary Oxides ($Ir-Ru-Ta-Sn$) | Dual Mixed Gas Evolution | 15.0 – 35.0 g/m² | < 6,000 A/m² | High-Chloride Acidic Wastewater, Complex Flue Gas Desulfurization Washwater |
Cathodic Protection (ICCP) Ribbon & Mesh
Navzo MMO titanium ribbon mesh and expanded mesh anodes deliver distributed current for reinforced concrete civil structures, tank bottom under-slab environments, and subsea pipelines. Certified for compatibility with calcined petroleum coke breeze backfills, ensuring zero passivation over decades of cathodic protection service.
Electrolytic Copper Foil for Lithium Batteries
In ultra-thin copper foil manufacturing (4.5µm to 6.0µm) for EV battery packs, anode shape stability and zero solution contamination are paramount. Our high-iridium $IrO_2-Ta_2O_5$ coated titanium arc anodes and mesh configurations eliminate lead sludge hazards and maintain uniform current density profiles across widths exceeding 1,400mm.
Advanced Water Oxidation & Disinfection
For treating refractory wastewater containing ammonia nitrogen, COD, and chlorinated pesticides, our boron-doped and noble-metal coated titanium mesh designs create secondary hydroxyl free radicals ($\cdot OH$). These achieve direct oxidation and mineralization of organics without requiring hazardous chemical flocculants.
Emerging Technology Trends in Titanium Mesh Anode Procurement
Strategic purchasing managers evaluate long-term shifts in raw material indices, coating life extensions, and next-generation green hydrogen electrolyzers.
1. Transition to Porous Transport Layers (PTL) for PEM & AEM Water Electrolysis
Global green hydrogen production relies heavily on titanium expanded mesh, sintered porous titanium sheets, and coated titanium felt. As proton exchange membrane (PEM) and anion exchange membrane (AEM) water electrolyzers scale to megawatt capacities, procurement demands are shifting from coarse diamond mesh to ultra-thin micro-expanded mesh (thickness ≤ 0.25mm, SWD ≤ 0.8mm) coated with sub-micron platinum or iridium-ruthenium layers to suppress interface resistance while preventing catalyst poisoning.
2. Nano-Composite Rare Earth Dopants ($CeO_2, ZrO_2, SnO_2$)
With global market prices for Iridium and Ruthenium experiencing market volatility, premier Chinese exporters are commercializing proprietary intermediate barrier layers and quaternary oxide cocktails doped with rare earths. By introducing nano-$CeO_2$ and $ZrO_2$ into the crystal matrix, coating grain boundary energy is reduced, curbing electrolyte permeation to the titanium baseplate and extending service life by 40% with reduced noble metal loading.
3. Complete Circular Recoating Economies
Environmental regulations and corporate ESG mandates have elevated stripping and recoating capabilities to top selection criteria for European and North American buyers. Titanium substrates remain physically intact after the catalytic oxide layer exhausts. Navzo provides comprehensive chemical dissolution protocols to strip depleted oxides without degrading substrate wall thickness, followed by surface reactivation and recoating—saving buyers 45% to 60% compared to purchasing virgin titanium units.
4. Automated Vision Systems & NDT Coating Thickness Validation
Manual tactile quality checks are being replaced by automated inline X-ray Fluorescence (XRF) spectrometry and non-destructive eddy current thickness gauges. International engineering contracts now mandate multipoint automated thickness mapping (ensuring nominal variance < 5% across 2m² panels) accompanied by digital Mill Test Certificates conforming to EN 10204 3.1 standards.
Navzo Precision Titanium: Why Global Engineers Partner With Us
Operating from Baoji High-Tech Development Zone since 2011. Bridging raw metallurgical advantage with strict western aerospace and electrochemical manufacturing tolerances.
Full Metallurgical Supply Security
Located directly within Baoji's world-renowned titanium industrial ecosystem, we control substrate traceability from sponge titanium melting to sheet rolling, slitting, drawing, precision stamping, and automated vacuum annealing, eliminating middle-tier trading markups.
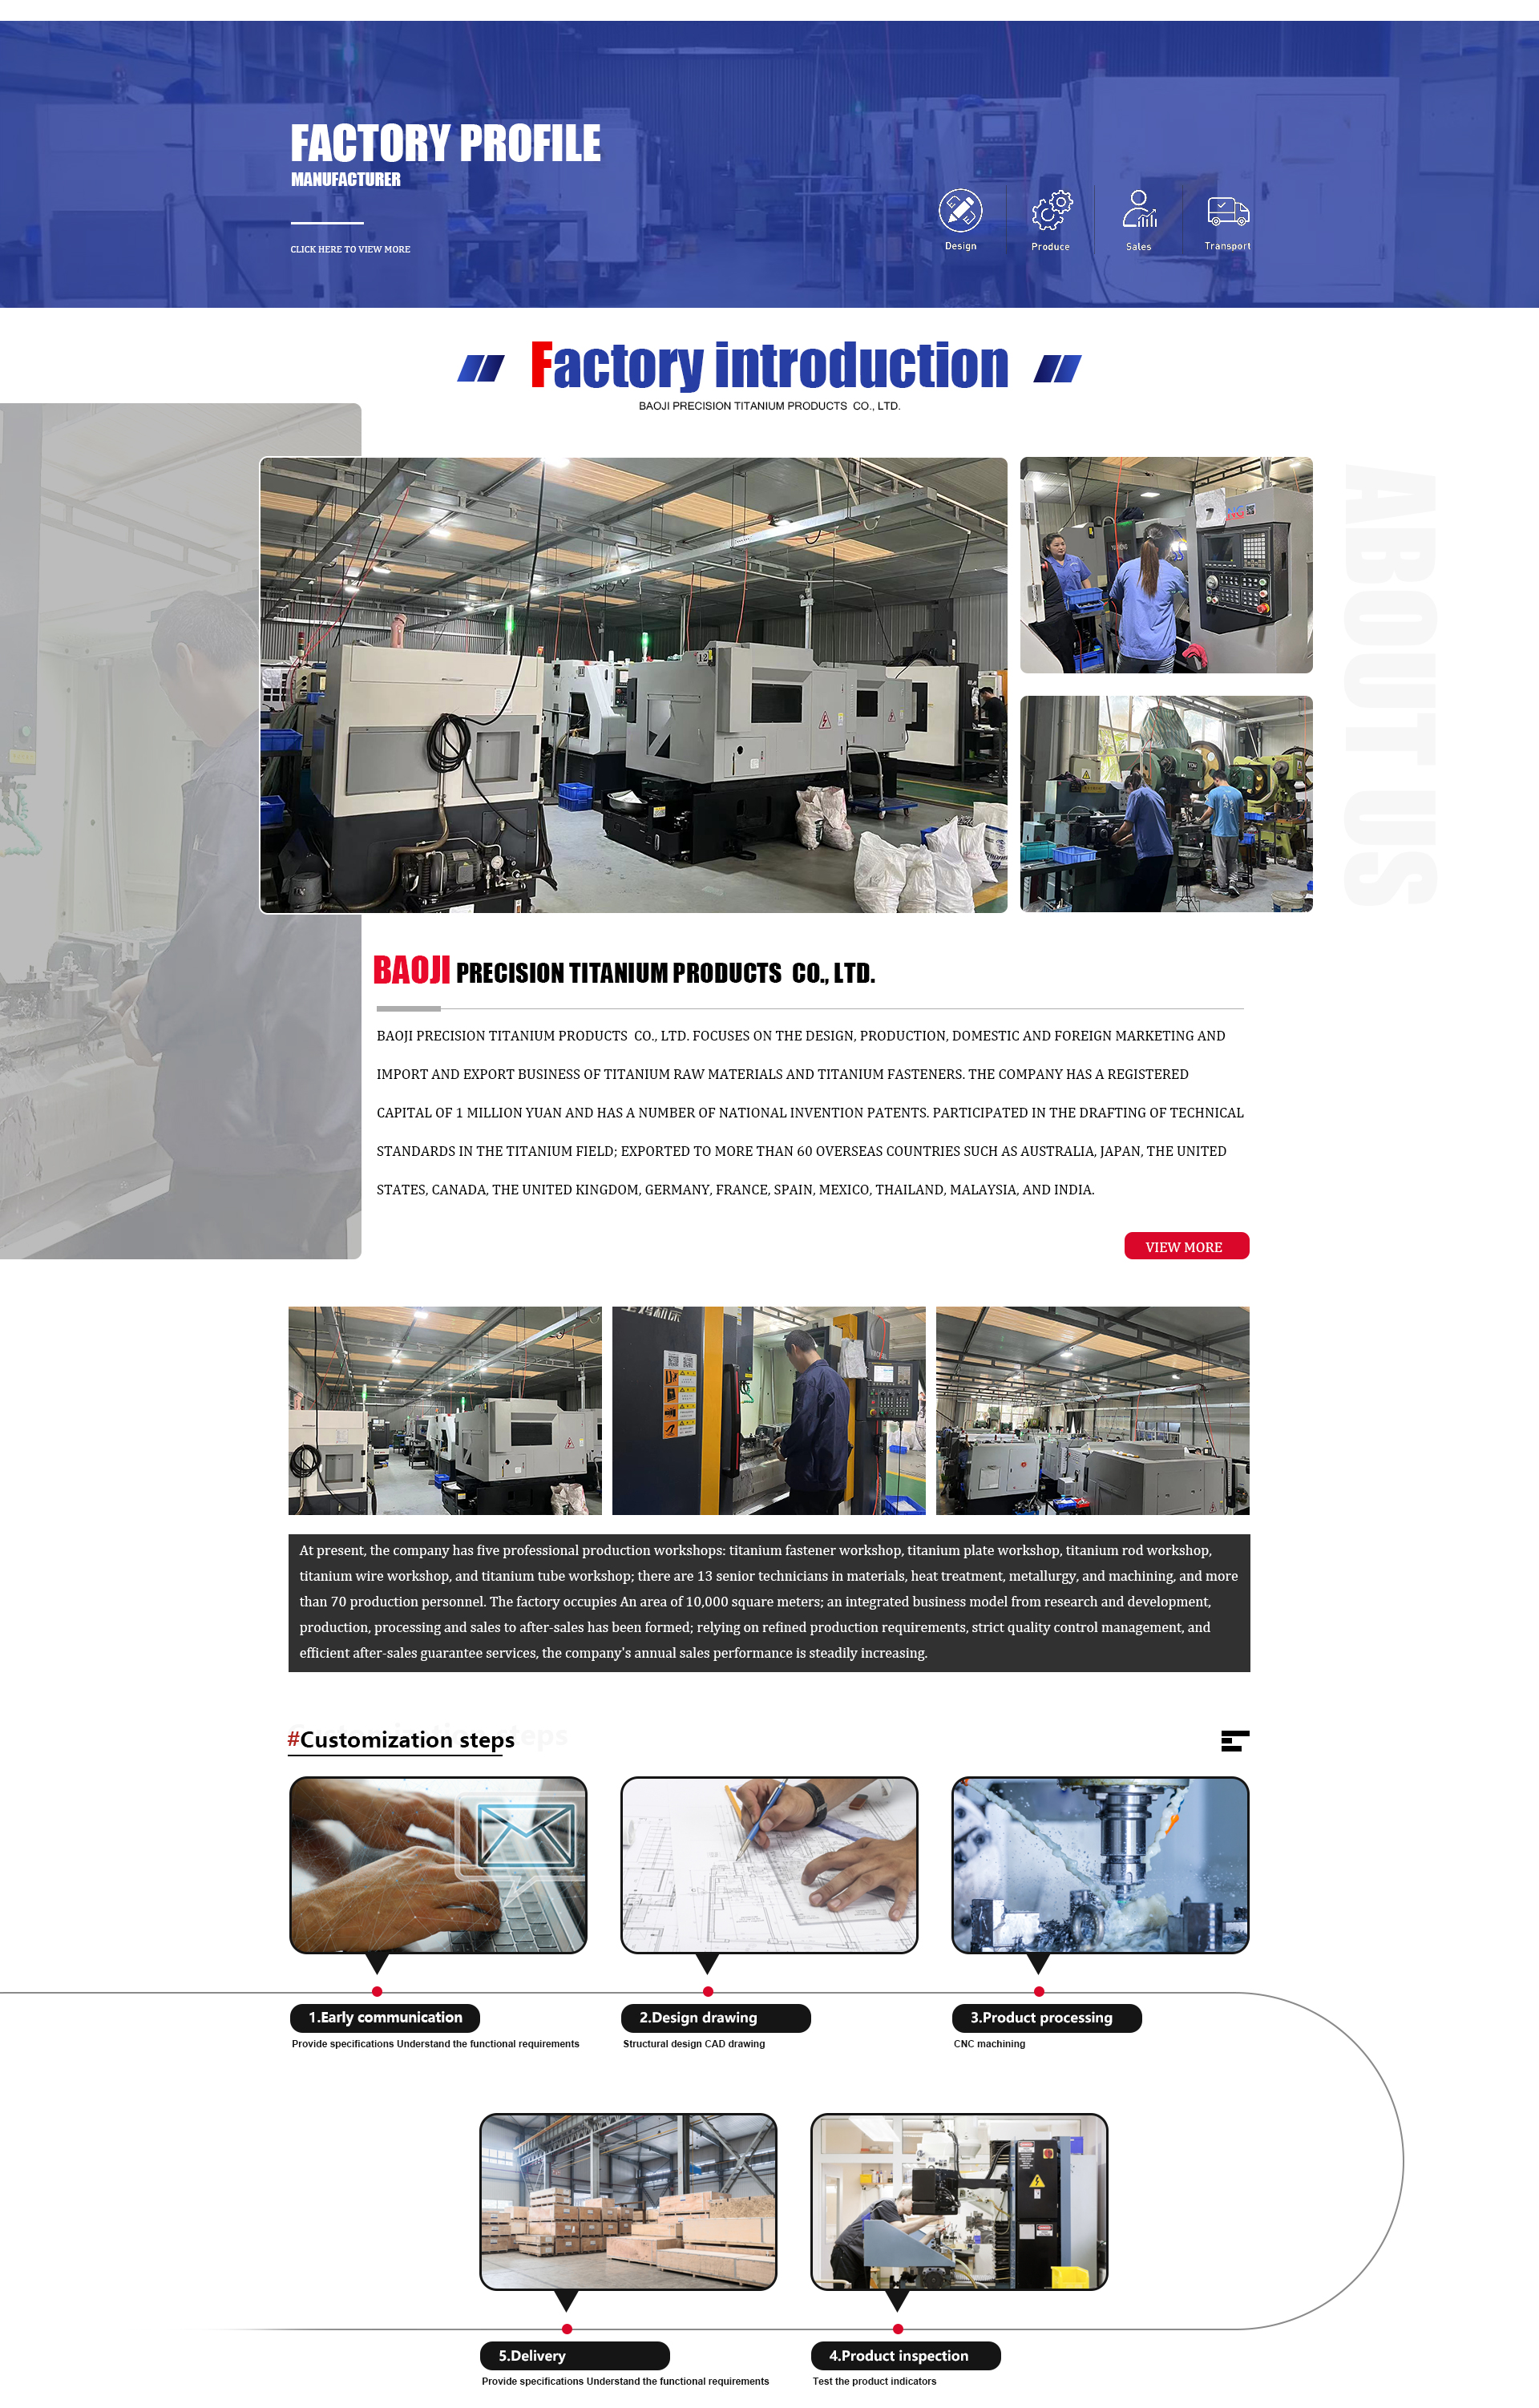
Precision Cold Heading & 5-Axis CNC
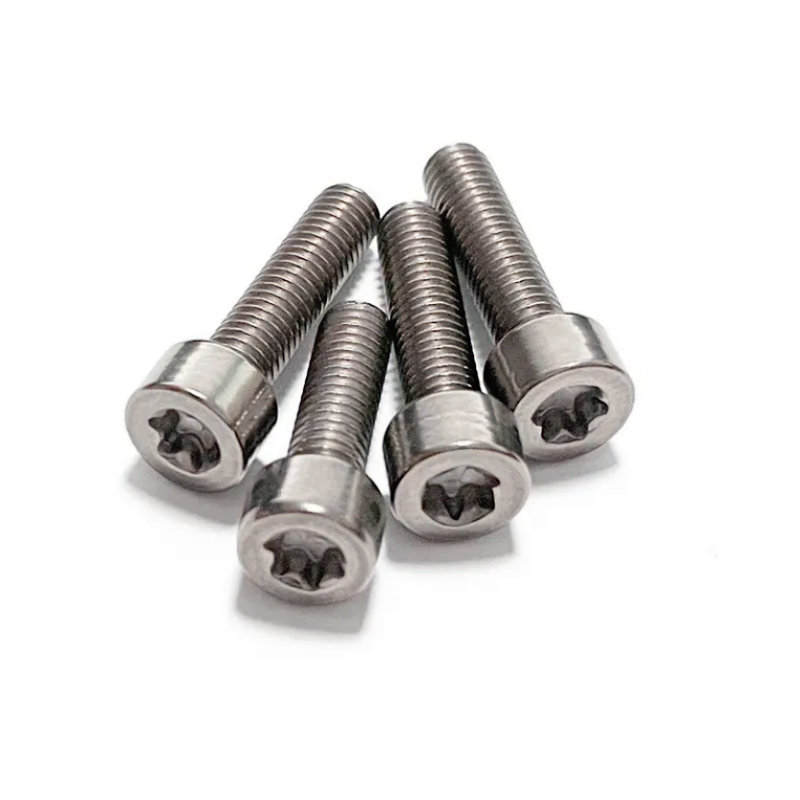
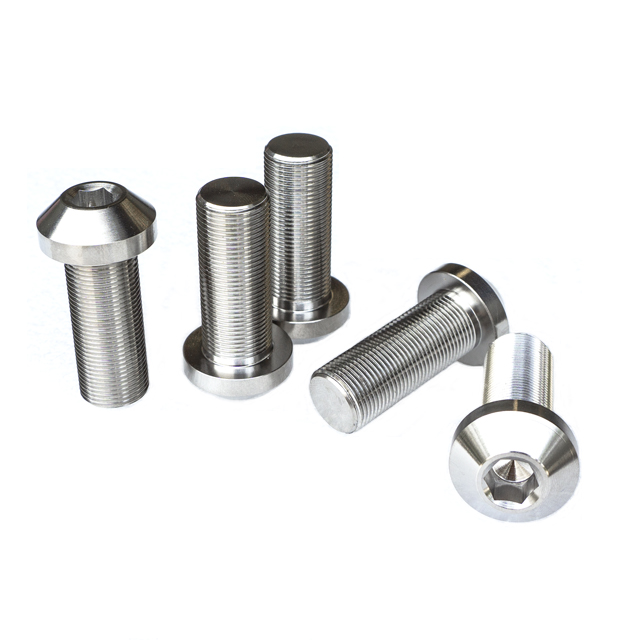
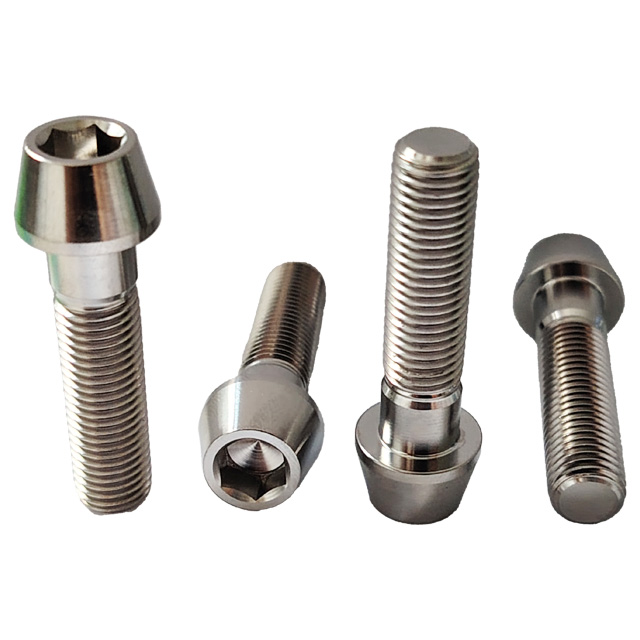
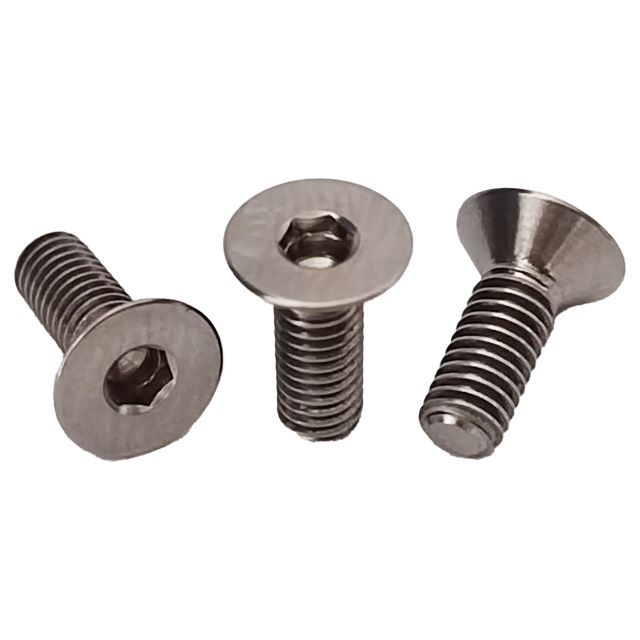
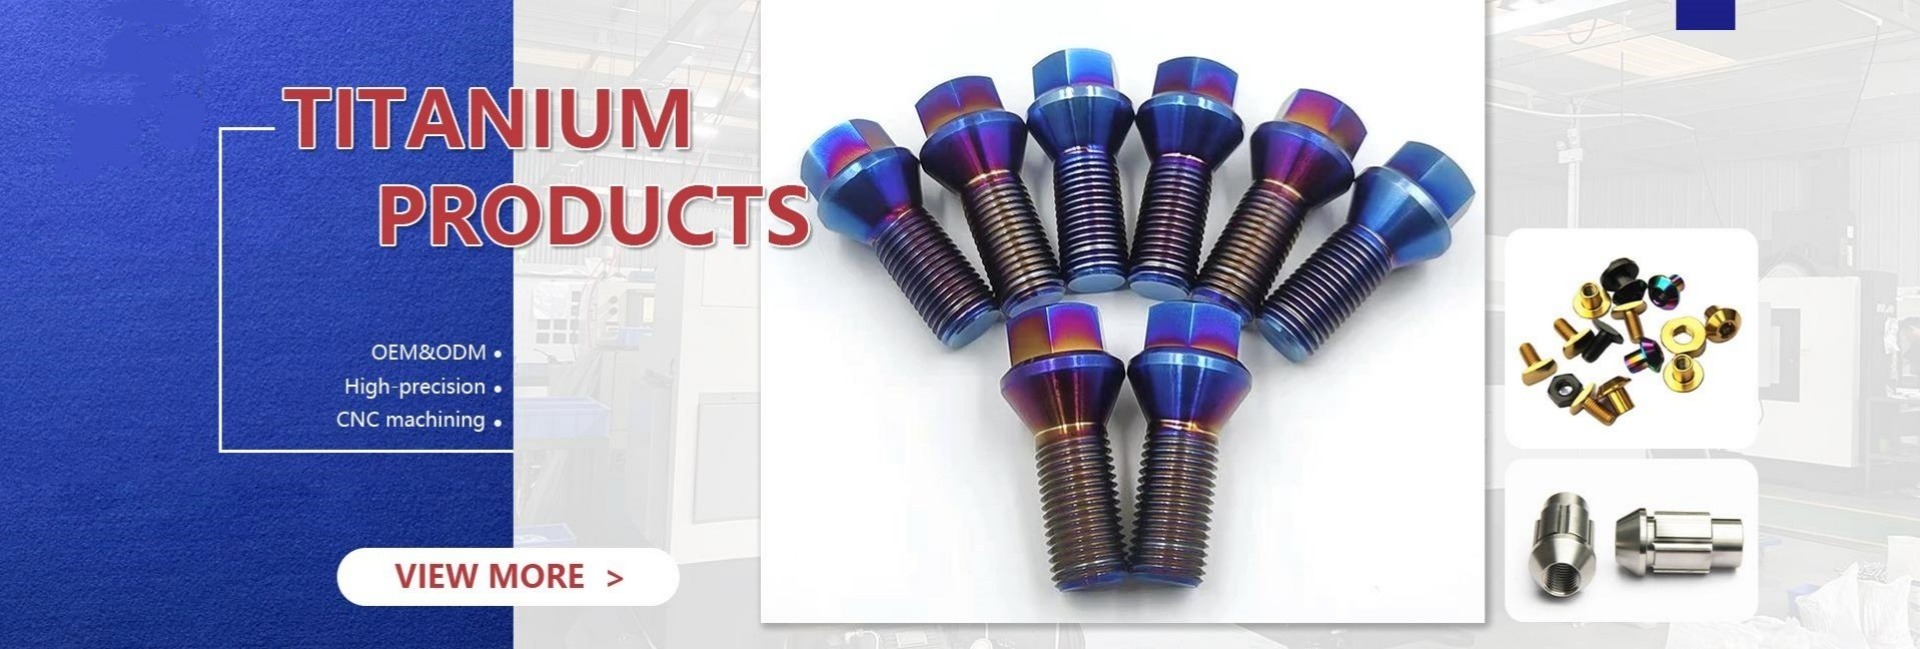
Beyond planar titanium mesh anodes, our facility houses high-speed cold heading machines, thread rolling equipment, and 5-axis CNC machining centers to manufacture titanium busbars, conductive hanging lugs, titanium fasteners (M3 to M36), and customized current distribution stems.
Rapid Response Engineering Culture
We maintain an average technical response time under 1 hour for global RFQs. Our senior metallurgical engineers review custom 2D/3D drawings (STEP, DWG, DXF, PDF), offering manufacturability feedback and alloy optimization before serial production runs.

Complete Manufacturing Chain Under One Roof
From initial titanium coil slitting and mesh expansion to automated acid etching cleaning lines, multiple thermal decomposition baking ovens, and rigorous coordinate measuring machine (CMM) inspections, Navzo manages the entire processing loop under strict ISO 9001:2015 quality standards.
Exporting to verified industrial clients across the United States, Germany, Russia, South Korea, Thailand, the Netherlands, and Japan, our documentation suite includes full material test reports (MTR), microscopic cross-section imaging, and certified chemical assays.

Frequently Asked Questions on Titanium Mesh Anodes
Comprehensive engineering clarifications covering chemistry, operating thresholds, coating lifetimes, and ordering specifications.
What is the difference between Grade 1 and Grade 2 titanium for anode substrates?
How is the lifetime of an MMO titanium mesh anode determined?
What critical factors cause premature deactivation of titanium mesh anodes?
1. Coating Dissolution: Gradual electrochemical consumption of active metal oxides.
2. Substrate Passivation: Electrolyte permeating through coating micro-cracks, forming a non-conductive titanium dioxide ($TiO_2$) dielectric barrier at the interface.
3. Mechanical Delamination: Inadequate surface sandblasting and acid etching prior to coating application.
4. Reverse Polarity / Short Circuits: Subjecting the anode to accidental cathodic polarization without proper protective interlocks.
Can Navzo customize anode mesh shapes, busbar connections, and mounting flanges?
What are the standard dimensions and tolerances for expanded mesh?
How does Navzo ensure noble metal coating loading and uniformity across large orders?
Do you offer substrate recoating services for international buyers?
What documentation is delivered alongside export shipments?
Request an Engineering Quotation for Titanium Mesh Anodes
Send your dimensional requirements, mesh geometry (LWD/SWD/Strand/Thickness), target electrolyte parameters, and required operating life. Navzo's electrochemical engineering team provides complete manufacturability reviews and competitive factory-direct pricing within one hour.