High-Performance Titanium Drivetrain & Sprocket Fasteners
Engineered from aerospace-certified Ti-6Al-4V Grade 5 alloy bar. Each bolt features cold-formed rolled threads and precision-machined drive sockets to withstand dynamic alternating shear loads in off-road, road racing, and industrial drivelines.
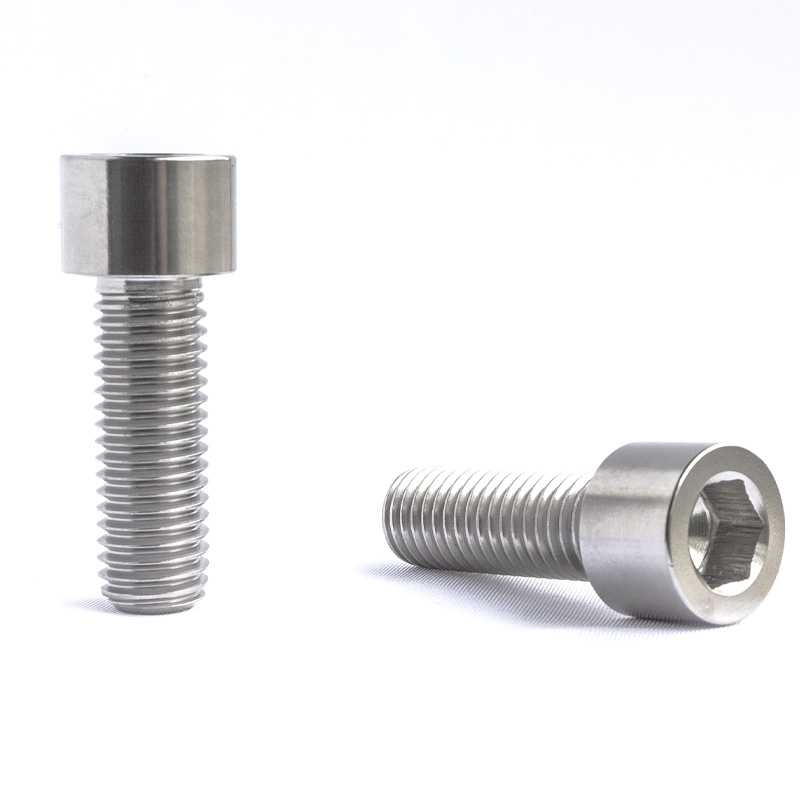
GR5 Titanium Bolts M12*45mm Hex Socket Cap Screws
- StandardDIN 912 / ISO 4762
- Thread Pitch1.25 / 1.50 mm Rolled
- Tensile Yield895 – 930 MPa
- Drive TypeInternal Hex Socket
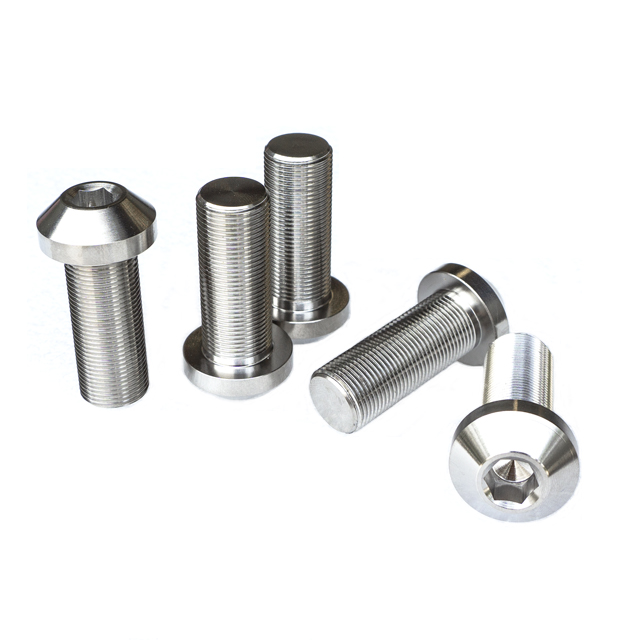
GR5 Titanium Bolts M14*1.0*35mm Umbrella Head Screws
- ConfigurationUmbrella / Conical Flange
- Thread PitchFine M14 × 1.0 mm
- Surface TechMicro-Polished / Raw
- ApplicationPrimary Shaft / Sprocket Hub
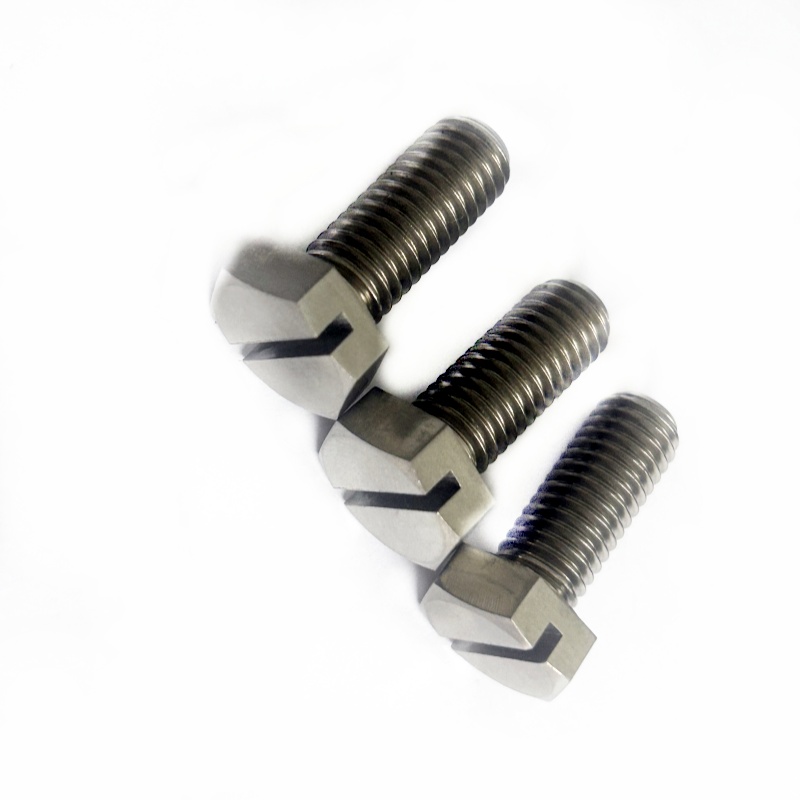
High Precision CNC Machined Slotted Hex Screw
- Machining Spec5-Axis Swiss Lathe Precision
- Tolerance±0.01 mm Strict Limits
- MaterialTi-6Al-4V Grade 5
- Safety DesignPre-Drilled Safety Wire Slot
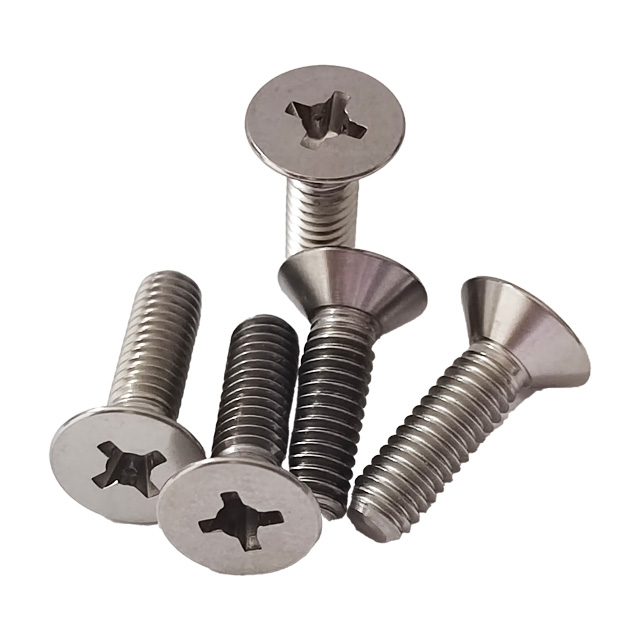
GR5 Titanium Bolts M8*20mm Countersunk Screws
- Head Geometry90° Flat Countersunk
- DriveReinforced Phillips / Cross
- Weight Saving45% vs Standard Alloy Steel
- InstallationFlush Rotor & Sprocket Retainers
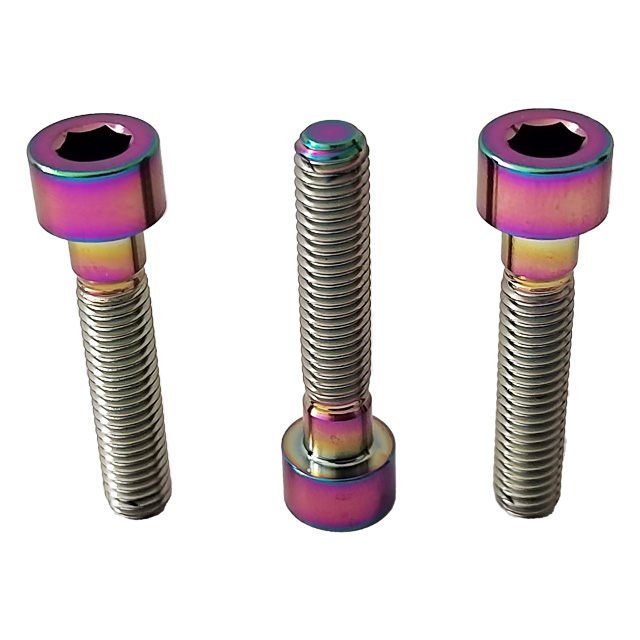
GR5 Titanium M8*40mm Colored Cylinder Socket Bolts
- CoatingElectrochemical Anodized / Burnt
- Thread PitchM8 × 1.25 Rolled Thread
- Corrosion RatingZero Salt-Spray Degradation
- Head StyleCylindrical Deep Hex Socket
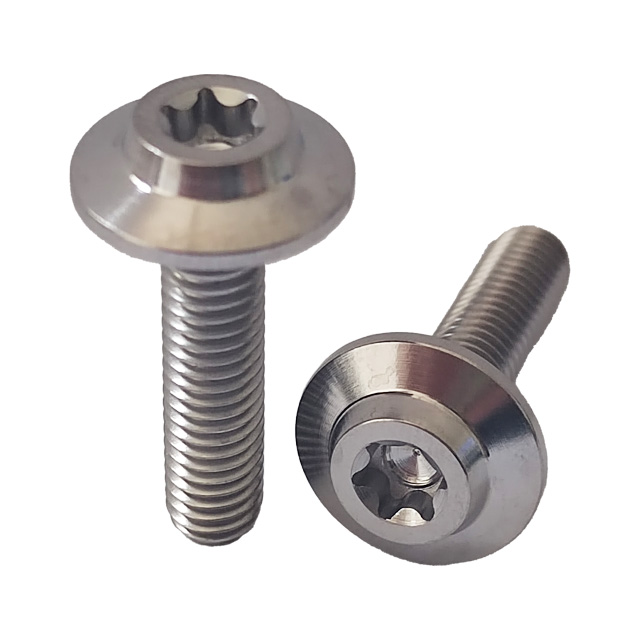
GR5 Titanium M6*25mm Umbrella Flange Torx Bolts
- Drive StyleInner Torx (Star) T30 Profile
- Head GeometryBroad Load-Dispersing Flange
- Torque CapacitySuperior Anti-Cam-Out Ratio
- Target UseChain Guides & Light Sprockets
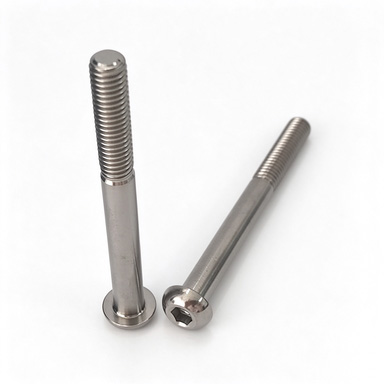
GR5 Titanium M6*70mm Button Head Inner Hex Screws
- Length / ShankExtra-Long 70mm Precision Shank
- Head ProfileLow-Drag Dome / Half-Round
- Fatigue Life>2,000,000 Cycle Dynamic Stress
- FinishNatural Bright / Vapor Blasted
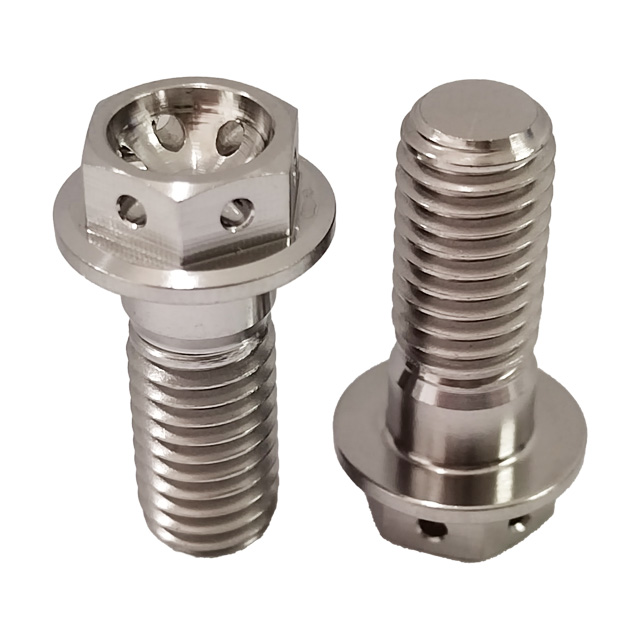
GR5 Titanium M8*20mm Drilled Hex Flange Bolts
- Security FeatureMulti-Hole Wire Lock Drilled
- Head StandardIntegral Flange Hex Head
- FitmentSuperbike / Motocross Rear Sprocket
- Torque Rating34 – 38 Nm Recommended Range
Dynamic Mechanics of Titanium Rear Sprocket Hardware
Why Tier-1 racing teams and factory OEM powertrain engineers transition from Grade 10.9/12.9 alloy steels to aerospace Ti-6Al-4V Grade 5 fasteners in high-torque drivetrains.
In modern performance motorcycles, rally quads, and electrified powertrains, the rear sprocket assembly constitutes an extreme operating environment characterized by high torsional impulse shocks, cyclic shear displacement, and high-frequency resonance. A typical 1000cc superbike or 450cc factory motocross machine delivers instantaneous peak torque spikes exceeding 1,200 Nm through the final drive chain directly to the rear hub interface. Standard carbon and alloy steel fasteners (such as ISO 898-1 Class 8.8 or 10.9), while possessing adequate raw tensile yield, contribute substantial parasitic rotating mass and are susceptible to catastrophic hydrogen embrittlement, stress-corrosion cracking, and galvanic corrosion when coupled with magnesium or 7075-T6 aluminum hubs.
"The kinetic energy stored in rotating unsprung driveline components scales with the square of radius and rotational velocity (E_rot = ½ I ω²). Substituting six M8×30mm steel sprocket bolts with Grade 5 Titanium reduces rotational inertia by 42.8%, directly translating into accelerated power transmission, diminished gyroscopic precession during corner transitions, and lowered shock fatigue on hub bearing journals."
— Navzo Technical Metallurgy & Fastener Testing Group1. Rolled Threads vs. Cut Threads: The Fatigue Life Imperative
A critical engineering failure mode in aftermarket titanium sprocket bolts is thread shear fatigue at the first engaged thread pitch. Low-cost manufacturers often manufacture titanium hardware via conventional subtractive CNC turning, cutting threads with a single-point carbide insert. This process severely disrupts the continuous grain flow of the metallurgical microstructure and induces micro-notches that act as acute stress concentrators under cyclic braking and acceleration loads.
In contrast, aerospace-grade manufacturing employs multi-station cold heading coupled with high-pressure cylindrical die thread rolling. Under cold plastic deformation, the alpha-beta grain boundaries of the Ti-6Al-4V alloy are compressed continuously along the flank, crest, and root radii. This creates deep residual compressive stresses at the root of the thread, elevating cyclic fatigue endurance by more than 35% to 45% compared to cut threads and entirely preventing micro-crack propagation under extreme dynamic chain tension.
| Fastener Material | Density (g/cm³) | Tensile Strength (MPa) | Yield Strength (MPa) | Shear Strength (MPa) | Corrosion Resistance | Drivetrain Suitability |
|---|---|---|---|---|---|---|
| Ti-6Al-4V (Grade 5 Titanium) | 4.43 | 950 – 1050 | 880 – 920 | 550 – 620 | Immune to atmospheric/salt | Optimal: Unsprung racing drivetrains |
| Commercially Pure Ti (Grade 2) | 4.51 | 345 – 480 | 275 – 350 | 240 – 310 | Exceptional | Unsuitable: Insufficient shear resistance |
| Medium Carbon Alloy Steel (Class 10.9) | 7.85 | 1040 | 940 | 620 | Poor (Requires zinc/nickel plating) | Standard OEM: High mass, prone to rust |
| Austenitic Stainless (A2-70 / 304) | 7.93 | 700 | 450 | 380 | Moderate | Hazardous: Low yield under shear torque |
| Aircraft Alloy Steel (Class 12.9) | 7.85 | 1220 | 1100 | 730 | Very Poor (Prone to embrittlement) | High tensile, but excessive rotating weight |
2. Tribological Interaction, Clamping Load, and Galling Prevention
Titanium exhibits an intrinsic affinity for oxygen, spontaneously generating an amorphous, passive TiO&sub2; ceramic oxide film. However, under high contact stresses during thread engagement, this delicate micro-film can break down, leading to direct metal-to-metal contact, local friction welding, and severe thread galling (seizure). To achieve consistent clamping preload (±5%) across all sprocket bolt holes, the following metallurgical and assembly protocols must be maintained:
Thread Lubrication & Friction Coefficients: Titanium bolts installed dry into female hub threads (or coupled with titanium flange locking nuts) display an unstable coefficient of friction (μ = 0.30–0.45), which absorbs applied torque without converting it into required axial clamping clamp load. Utilizing an anti-seize paste containing copper, aluminum, or molybdenum disulfide (MoS&sub2;) stabilizes friction at μ = 0.12–0.14. This ensures that a torque setting of 35 Nm delivers precisely 22.4 kN of axial clamping load, clamping the sprocket firmly to the wheel hub face and preventing microscopic rocking or shear slop that causes hole elongation.
Top 10 Titanium Sprocket Bolts Manufacturers & Suppliers
A rigorous industry benchmark evaluating production infrastructure, raw material traceability, cold heading capabilities, dimensional quality controls, and OEM supply reliability.
Navzo Precision Titanium Products Co., Ltd.
Founded in 2011 in the epicenter of China's titanium metallurgy cluster, Navzo is an elite ISO9001-certified manufacturer specializing in high-tensile Gr5 (Ti-6Al-4V) drivetrain hardware, rolled-thread racing bolts, and CNC custom titanium components. Featuring direct-mill ingot sourcing, cold heading, and precision vacuum coating.
- Fully integrated Baoji melt-to-part traceable supply
- Cylindrical cold-die thread rolling for zero fatigue failure
- Rapid 1-hour engineering quote turnaround & OEM ODM
Pro-Bolt
Recognized worldwide as a high-end aftermarket motorsport fastener supplier, Pro-Bolt provides titanium hardware directly to teams in MotoGP, World Superbike, and British Superbikes. Their catalog covers tailored motorcycle sprocket bolt sets with drilled flange heads.
- Extensive race team sponsorship footprint
- Pre-packaged model-specific retail kits
- High premium unit pricing on aftermarket sets
Racebolt UK
Racebolt operates in-house CNC machining centers in the UK dedicated to motorcycle racing fasteners. They offer precision machined sprocket bolts, brake rotor kits, and caliper mount hardware utilizing Grade 5 titanium with an emphasis on race safety lock-wiring features.
- In-house CNC lathe manufacturing in the UK
- Specialized drilled safety lock-wire heads
- Strong presence in Isle of Man TT paddocks
Lunsford Racing
A legendary US manufacturer with decades of expertise in Grade 5 titanium turnbuckles, axles, and specialty lightweight fasteners. Originally serving off-road RC and competitive motocross, Lunsford utilizes domestically certified US titanium bars with tight shank runout controls.
- 100% USA milled titanium bar stock
- Highly reputed in off-road competition sectors
- Specialized batch production runs
Mettec Titanium Fasteners
Mettec is an American pioneer in hot-forged and rolled thread titanium hardware for aerospace, defense, and top-tier auto/moto racing. Their sprocket and driveline bolts feature tight concentricity and mil-spec certifications complying with AMS 4928 parameters.
- Aerospace-grade hot-heading forging equipment
- Strict quality verification for defense & aerospace
- Focus on industrial contracts and bulk orders
Ti64 Titanium
Positioned at the heart of American stock-car racing, Ti64 manufactures titanium fasteners engineered for high-shear sprint car hubs, motorcycle swingarms, and driveline assemblies. They provide specialized 12-point flange heads and countersunk sprocket hardware.
- Specialized 12-point aerodynamic flange designs
- High shear fatigue testing verification
- Strong US sprint car and track day presence
Ticon Industries
Renowned for motorsport titanium fabrication components, Ticon has developed a dedicated lineup of drivetrain and wheel-hardware fasteners. Their Grade 5 titanium sprocket stud kits and locking nuts are favored by custom sportbike and drag-racing builders.
- Precision thread tolerance matching
- Integrated stud conversion hardware sets
- Broad distributor reach throughout the Americas
Supersprox Hardware
As a world leader in high-performance hybrid motorcycle sprockets (Stealth), Supersprox designs and supplies bespoke titanium mounting hardware engineered strictly to mate with their sprocket drive flanges and OEM hub counterbores.
- Direct compatibility with performance sprockets
- Deep mechanical knowledge of final-drive torque dynamics
- Focused catalog tailored purely to sprockets
TitanX Motorsport Fasteners
TitanX focuses on precision DIN and ISO standard titanium fasteners for German touring car teams, endurance racing, and high-output electric superbikes. Their sprocket bolts undergo mandatory eddy-current non-destructive flaw detection.
- 100% Eddy-current and ultrasonic non-destructive testing
- Strict adherence to DIN EN 9100 aerospace standards
- Targeted primarily at European racing series
Acerbis Motorsport Hardware Division
Acerbis' racing division supplies European motocross, Dakar rally teams, and OEM factory teams with turnkey hardware assemblies. Their titanium off-road sprocket bolt kits feature tapered underheads with interlocking Fuji-style all-metal locking nuts to resist the aggressive vibration and mud buildup encountered in world championship off-road rallies.
- Specialized off-road vibration damping geometries
- Paired with all-metal prevailing-torque locknuts
- Broad off-road motorcycle OEM distribution network
Why Navzo Leads Global Titanium Fastener Procurement
Located on Yucai Road, High-tech Development Zone, Baoji, Shaanxi — China's "Titanium Valley" — Navzo provides an uncompromised supply chain advantage from raw certified titanium sponge to high-precision finished bolts.
Direct Baoji Cluster Integration
Baoji manufactures over 60% of China's and 20% of the world's titanium bar and sponge. Operating directly inside this industrial cluster eliminates raw-material brokerage layers, guaranteeing 100% chemically traceable Ti-6Al-4V stock with Mill Test Reports (MTR) according to ASTM B348 and AMS 4928 standards.
Complete Internal Production Chain
Navzo avoids fragmented outsourcing. Our factory floor houses multi-station high-speed cold headers, Japanese multi-axis Swiss CNC turning centers, hydraulic cylindrical thread rollers, and computer-controlled ultrasonic cleaning systems, ensuring dimensional tolerances within ±0.008 mm on critical shank diameters.
Advanced PVD & Anodizing Facilities
Equipped with automated electrochemical color anodizing tanks and high-vacuum Physical Vapor Deposition (PVD) chambers. We deposit high-hardness titanium nitride (TiN), titanium carbonitride (TiCN), burnt blue gradient finishes, and Diamond-Like Carbon (DLC) coatings with superior scratch and fretting resistance.
Future Procurement & Technological Trends (2025–2030)
Market forecasting for supply chain managers, automotive component buyers, and race team technical directors navigating global titanium fastener demand.
Shift to Multistation Cold-Forged Head Geometry
Rising titanium raw bar costs are accelerating the phase-out of pure CNC subtractive milling for standard bolts. High-volume procurement is transitioning toward high-speed multi-station cold-heading machines. This manufacturing method minimizes scrap rate from 65% down to under 8%, lowering unit purchase cost by 28% while simultaneously enhancing grain structure flow across the bolt head-to-shank transition fillet.
Surge in High-Output Electric Supermoto Drivetrains
Electrified dirt bikes and road motorcycles (e.g., Stark VARG, Zero, Ducati MotoE prototypes) generate zero-RPM peak electric torque, producing severe shock loads that exceed conventional internal combustion engines by over 40%. Procuring procurement teams are mandating Grade 5 titanium rear sprocket bolts with larger M10 flange interfaces, replacing vintage M8 hardware to prevent instantaneous shear snapping.
Dry-Film Anti-Galling & DLC Hard Coatings
Environmental workplace regulations and racing pit stop speed demands are driving the obsolescence of manual wet molybdenum anti-seize paste. Manufacturers are implementing vacuum-deposited MoS&sub2;-doped DLC coatings or plasma electrolytic oxidation (PEO). These micro-coatings provide lifelong, dry lubrication with stable friction coefficients (μ = 0.10) directly out of the box, completely neutralizing titanium galling.
B2B Digital RFQ & Mill-to-Assembly Supply Transparency
Procurement departments are abandoning non-verified third-party trading intermediaries in favor of direct factory engagements offering live video factory audits, full spectrometer chemistry verification reports, and digital 3D CAD step-file integration. Direct communication with engineering hubs like Navzo enables rapid custom prototyping and pre-production tolerance verification in under 48 hours.
Frequently Asked Questions: Titanium Sprocket Bolt Sourcing
Clear, uncompromised answers to the technical, metallurgic, and commercial questions asked by professional procurement engineers.
Why is Grade 5 (Ti-6Al-4V) strictly specified over Grade 2 for sprocket bolts?
What torque values should be applied to M8 Grade 5 titanium sprocket bolts?
Should threadlocker (Loctite) or anti-seize lubricant be applied?
How do you prevent galvanic corrosion between titanium bolts and aluminum hubs?
What is the Minimum Order Quantity (MOQ) and production lead time at Navzo?
What quality verification and metallurgical certificates accompany every shipment?
Direct Factory Procurement & Custom Engineering
Request comprehensive wholesale price lists, 3D STEP drawings, custom OEM machining quotations, or mill test verification certificates directly from our senior titanium engineering team in Baoji.