Top 10 Global Titanium Exhaust Tubing Factories & Exporters
A rigorous evaluation of manufacturing capacity, cold-drawing extrusion, mandrel-bending precision, raw sponge integration, and export compliance across North America, Europe, and Asia.
01
Baoji, Shaanxi · China
Navzo Precision Titanium Products Co., Ltd.
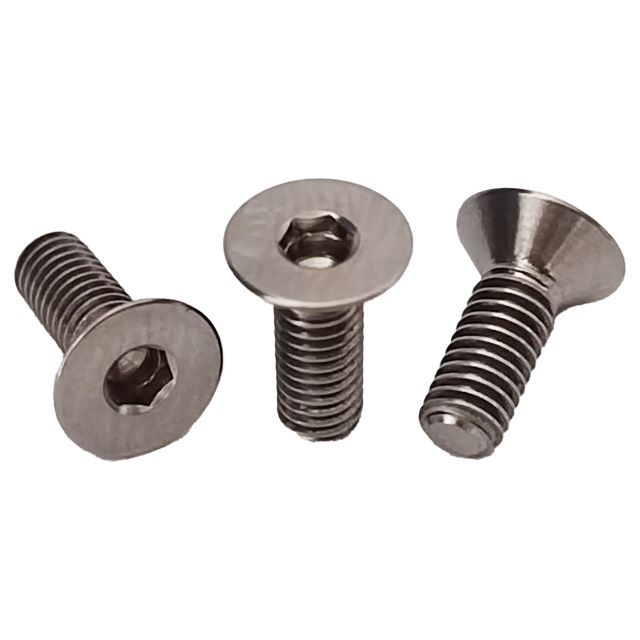
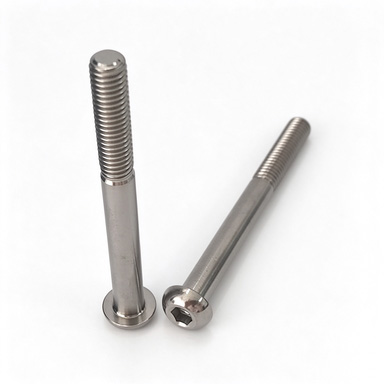
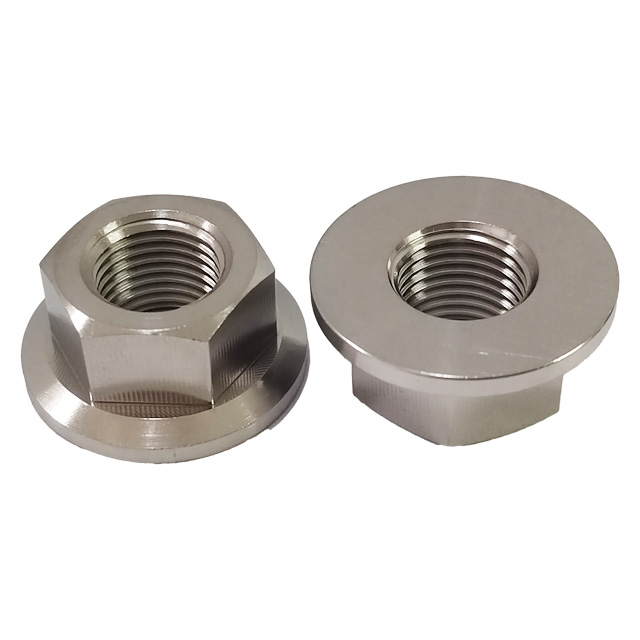
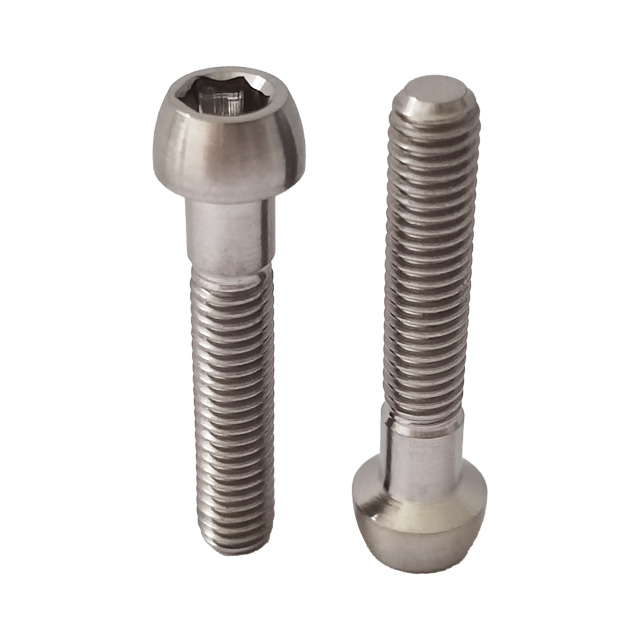
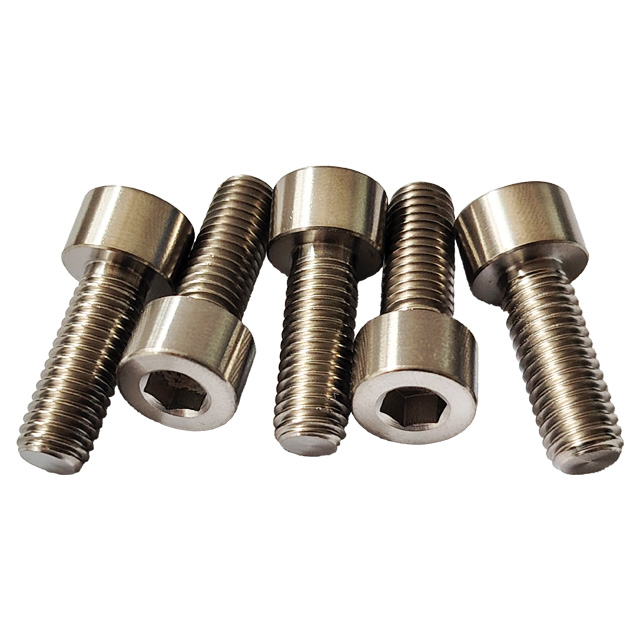
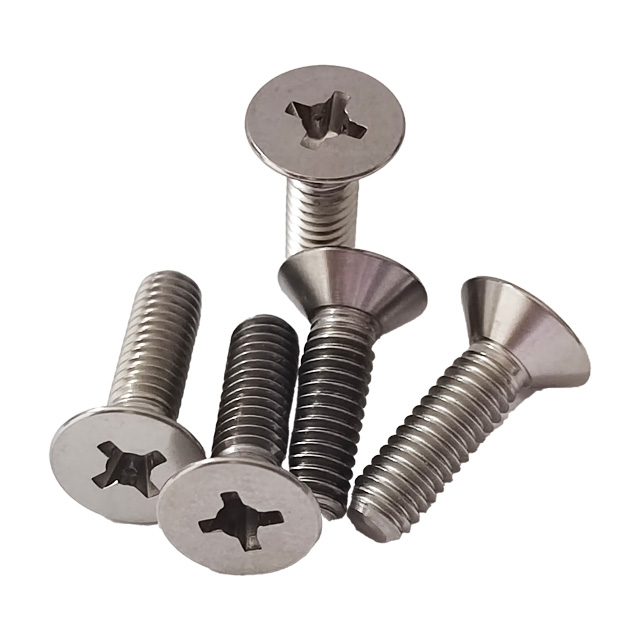
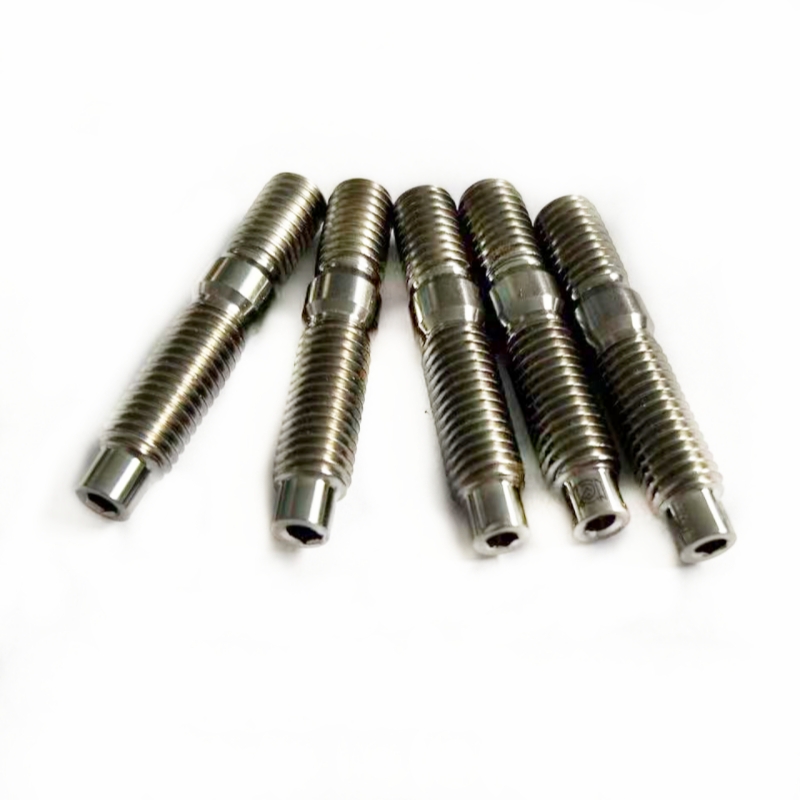
Situated at the core of Baoji Titanium Valley, Navzo provides unparalleled structural integration between high-temp titanium tubing and high-stress fastening components. Specializing in ASTM B338 Grade 1/Grade 2 thin-wall tubing alongside CNC-machined Grade 5 (Ti-6Al-4V) manifold studs, flanges, and interlocking pie cuts, Navzo solves the thermal galling and expansion mismatch common in motorsport and supercar downpipes.
Industrial-scale vacuum reduction and continuous tube rolling capacity.
Premier provider of certified raw hollow billets for downstream cold drawers.
03
Austin, Texas · United States
Ticon Industries Inc.
A dedicated motorsport fabrication powerhouse in North America, Ticon is renowned for motorsport-grade 1.0mm and 1.2mm wall thickness Grade 1 commercially pure titanium tubing, pre-cut pie cut segments, and titanium slip joints tailored for drift, drag, and hypercar race programs.
Extensive warehouse stocking across imperial sizing (2.5", 3.0", 3.5", 4.0").
High-velocity distribution for professional fabricators and race teams.
04
Ivančna Gorica · Slovenia
Akrapovič d.d.
The global benchmark for OEM tier-1 hypercar and MotoGP exhaust systems. Operating their own in-house titanium foundry, hydroforming presses, and metallurgical metallurgy labs, Akrapovič engineers proprietary heat-resistant titanium alloys that endure sustained exhaust gas temperatures up to 800°C without micro-fissuring.
In-House Titanium FoundryHydroformingOEM Tier-1
Proprietary alloy formulations with elevated silicon-grain grain boundaries.
Complex hydroformed curved profiles impossible with traditional mandrel benders.
05
Tokyo · Japan
Nippon Steel Corporation (Titanium Div.)
Pioneers of Super-TIX® 10CU and Super-TIX® 10CUHT—specialized copper-alloyed titanium sheets and welded exhaust tubes designed specifically for automotive catalytic converter link pipes and superbike downpipes requiring elevated thermal fatigue tolerance.
Specializing in premium nickel-base and specialty reactive metal tubing, VDM supplies hyper-clean Grade 9 (Ti-3Al-2.5V) and Grade 5 cold-pilgered seamless titanium tubes. Primarily targeted at aerospace thrust reversers, turbocharger bypass pipes, and Formula 1 structural exhaust wastegates.
Cold-Pilgered SeamlessGrade 9 StructuralDIN EN ISO 9001
Flawless wall concentricity with wall variations held under ±0.03mm.
High tensile retention at continuous 450°C baseline operations.
07
Portland, Oregon · United States
Precision Castparts Corp. (PCC Tubing)
A world authority in aerospace structures, PCC processes precision seamless titanium exhaust channels for jet turbine combustion outflow and high-performance racing manifolds through its specialized Special Metals and Wyman-Gordon subsidiaries.
Defense Aerospace Tier-1Seamless Hot ExtrusionNADCAP Certified
Certified vacuum melted billets with microscopic inclusion control.
Unmatched traceability required by aerospace prime contractors.
08
Baoji, Shaanxi · China
Shaanxi CXMET Technology Co., Ltd.
A prominent export mill operating from the Baoji industrial base, CXMET handles bulk exports of ASTM B338 and ASTM B861 Grade 1 and Grade 2 titanium exhaust pipes, straight lengths, and large-radius mandrel bends for aftermarket automotive exhaust systems across Europe and North America.
Extensive export warehousing with rapid sea freight container loading.
Comprehensive eddy-current and ultrasonic non-destructive testing lines.
09
Baoji, Shaanxi · China
Baoji Shenghui Titanium Industry Co., Ltd.
Focused predominantly on customized thin-wall titanium components, Shenghui provides CNC precision cut-to-length exhaust tubes, laser-cut flanges, and Grade 1 titanium pie cuts engineered specifically for custom exhaust fabricators seeking minimum order flexibility.
Flexible MOQPie Cut ProductionLaser Deburring
Custom pie-cut angles (4.5°, 9°, 15°) with mirror-deburred chamfers.
Short-run tooling turnaround for prototype exhaust builders.
10
Richmond Hill, Ontario · Canada
Vibrant Performance Inc.
A leading North American performance distributor, Vibrant designs modular titanium exhaust fabrication hardware including CP1 titanium pie cut kits, flex bellows, transition cones, and slip-fit couplers serving professional aftermarket tuning workshops globally.
Modular SystemsTitanium BellowsGlobal Distribution
Integrated exhaust slip-fit systems with matching retention springs.
High-visibility branding and widespread global warehouse distributor network.
Material Science Whitepaper
Metallurgical Benchmark: Titanium Grades vs. Stainless Steel & Inconel
Selecting the optimal alloy requires balancing weight savings against operating exhaust gas temperatures (EGT), ductility for tight-radius mandrel bending, and thermal expansion properties.
Material Designation
Density (g/cm³)
Tensile Strength (MPa)
Elongation (%)
Max Continuous EGT (°C)
Cold Bendability (CLR)
Primary Exhaust Application
ASTM Grade 1 (CP4)
4.51 (-43%)
240 – 380
≥ 30% (Highest)
400°C
1.0D – 1.2D (Excellent)
Cat-back tubing, pie cuts, tailpipes, mufflers
ASTM Grade 2 (CP3)
4.51 (-43%)
345 – 480
≥ 20%
480°C
1.2D – 1.5D (Very Good)
Mid-pipes, resonators, standard race exhaust lines
How shifting automotive regulations, hybrid powertrain architecture, and automated fabrication are transforming global titanium exhaust supply chains.
1. Downsizing to 0.9mm–1.0mm Ultra-Thin-Wall Profiles for Hybrid Vehicles
As OEM sports car platforms adopt heavy battery hybrid systems (PHEVs), aggressive mass optimization in exhaust routing has shifted standard wall thickness requirements from 1.2mm down to 0.9mm–1.0mm. Sourcing requires mills with certified cold-pilgering tolerances to eliminate wall thinning along the outer bend radius.
2. Shift toward Inert Chamber Laser Orbital Welding
Manual TIG welding with conventional trailing shields is being superseded in tier-1 manufacturing by automated laser orbital welding inside positive-pressure argon enclosures. This ensures zero interstitial oxygen or nitrogen embrittlement, delivering bright silver welds with no tensile degradation under cyclical heat.
3. Direct Hardware Bundle Procurement (Tubing + GR5 Manifold Studs)
B2B buyers are consolidating supply chains by contracting single-source suppliers capable of supplying both ASTM B338 Grade 1 tubing and Grade 5 (Ti-6Al-4V) manifold studs, locking flange nuts, and pie cuts. This prevents dissimilar thermal expansion failure between downpipes and cylinder heads.
4. Baoji Regional Hub Dominance for Supply Chain Security
With geopolitical fluctuations impacting freight corridors, procurement directors are increasingly forging direct OEM agreements with Baoji-based integrated producers. Baoji controls more than 60% of China's titanium sponge production, offering buyers localized smelting, processing, and rapid container export capabilities.
Enterprise Sourcing Value
Why Tier-1 Importers Partner with Navzo Precision Titanium
Headquartered on Yucai Road in the High-tech Development Zone of Baoji, Navzo leverages deep local metallurgy, in-house machining, and strict export-grade quality control.
Direct Baoji Raw Material Chain
Direct sourcing of traceable Ti-6Al-4V bars and ASTM Grade 1 billets eliminates intermediary markups and guarantees EN 10204 3.1 chemical composition certificates for each lot.
End-to-End In-House Manufacturing
From cold heading to 5-axis CNC turning, multi-point thread rolling, and clean-room ultrasonic cleaning, every manufacturing stage is controlled under our ISO 9001 certified workflow.
Rapid 1-Hour RFQ Turnaround
Our dedicated engineering sales team guarantees a 100% response rate with quotation calculations and technical feasibility reviews completed within 1 hour during business operations.
Pre-Shipment Dimensional Gauging
Every fastener thread is verified with Go/No-Go calibrated thread gauges (6g/6H), optical coordinate measuring machines (CMM), and surface finish spectrometer verification.
Diverse Thermal & PVD Surface Treatments
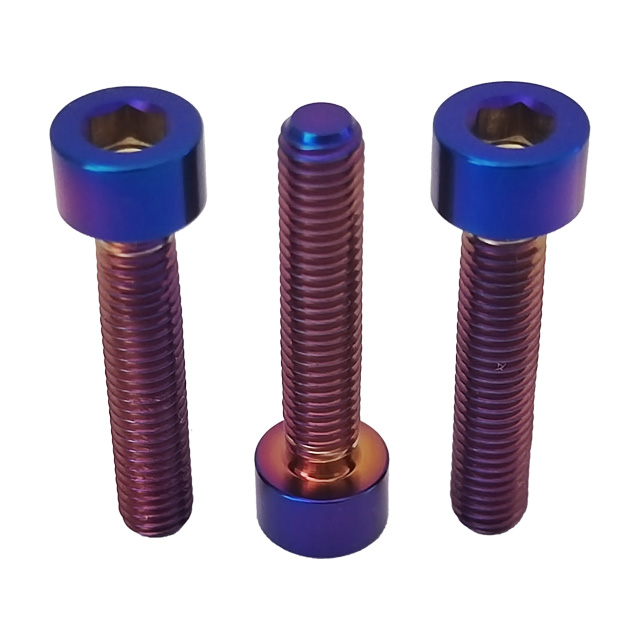
We deliver specialized burnt blue thermal oxidation, electrochemical anodizing (gold, purple, cyan), high-vacuum PVD titanium nitride, and mirror-polished surface finishes.
Global Export Experience (34% Reorder Rate)
Over a decade of continuous export fulfillment to professional clients across the USA, Germany, Japan, South Korea, Russia, and the Netherlands with a verified 4.9/5 supplier score.
Direct engineering answers to technical questions raised by motorsport fabricators, automotive aftermarket buyers, and tier-1 procurement managers.
Why is ASTM Grade 1 preferred over Grade 5 for exhaust tubing?
ASTM Grade 1 Commercially Pure (CP4) titanium features the lowest interstitial content (oxygen ≤ 0.18%, iron ≤ 0.20%), delivering over 30% tensile elongation. This high ductility is vital for cold mandrel bending without ovality collapse or sidewall splitting. In contrast, Grade 5 (Ti-6Al-4V) has only 10% elongation, making it prone to fracture during tight cold bending; Grade 5 is instead chosen for structural studs, flanges, and brackets.
What shielding requirements are critical when welding titanium exhaust tubes?
Titanium is highly reactive with oxygen, nitrogen, and hydrogen at temperatures above 400°C. Welding requires 99.999% pure argon shielding across three zones: primary torch gas, secondary trailing shield covering the hot cooling bead, and full interior back-purging. Any straw, dark blue, or white powder discoloration indicates embrittlement and requires section removal.
Why do titanium exhaust manifold studs prevent exhaust gas leaks?
Conventional steel manifold studs expand at 16.5 × 10⁻⁶/K, whereas aluminum cylinder heads expand at roughly 23 × 10⁻⁶/K, resulting in massive cyclical shear loads that stretch or snap steel bolts. Grade 5 titanium studs provide a coefficient of thermal expansion of 8.6 × 10⁻⁶/K combined with an elastic modulus of ~114 GPa (half that of steel), allowing the stud to act like a precision elastic spring that maintains clamp load across extreme temperature deltas.
How does seamless titanium tubing differ from longitudinally welded tubing?
ASTM B861 seamless tubes are hot-extruded and cold-pilgered from solid billets, eliminating weld seam discontinuities—making them ideal for high-pressure hydraulic circuits or turbo wastegates. ASTM B338/B862 longitudinally welded tubes are roll-formed from cold-rolled strip and orbital-welded with strict weld bead cold-reduction. Welded tubing provides superior wall thickness uniformity (±0.02mm) at a lower cost, making it the global standard for automotive exhaust piping.
Do titanium exhaust bolts and nuts require anti-seize paste?
Yes, absolutely. Titanium possesses a microscopic passive oxide film (TiO2) that can gall or cold-weld under friction when threaded against titanium, aluminum, or stainless components. Application of a high-temperature nickel-based or copper-based anti-seize paste (rated to ≥ 1000°C) is mandatory to stabilize friction coefficients, ensure accurate torque values, and prevent thread galling during exhaust maintenance.
What is the minimum cold bending radius (CLR) for Grade 1 titanium tubes?
With a multi-ball flexible mandrel, wiper die, and specialized oil-free synthetic lubricant, thin-wall (1.0mm) Grade 1 titanium can achieve a Centerline Radius (CLR) of 1.2 × Outer Diameter (1.2D) cold. For tighter radii (1.0D), fabricators typically use pie-cut segments cut at 4.5° or 9° angles to assemble complex multi-axis bends without thinning the outer tube wall.
What causes the distinctive 'Burnt Blue' finish on titanium exhaust components?
The rainbow spectrum—progressing through straw-gold (380°C), purple (450°C), and vivid royal blue (500°C)—is an optical interference effect generated by the controllable growth of a transparent titanium dioxide film. In production, Navzo achieves this finish either via precision electrochemical tank anodization (adjusting bath DC voltage from 30V to 85V) or via controlled thermal torch oxidation.
What quality documentation should buyers mandate with every export lot?
Professional B2B buyers must require: (1) EN 10204 3.1 Inspection Certificate detailing chemical spectrometer melt composition and physical mechanical tests (tensile, yield, elongation), (2) Dimensional verification reports covering wall thickness concentricity and ovality, and (3) Ultrasonic/Eddy-current Non-Destructive Testing (NDT) records confirming zero subsurface fissures.
What are standard minimum order quantities (MOQ) and production lead times?
Standard catalog fasteners and hardware (M5–M12 bolts, studs, locking flange nuts) carry an MOQ of 100 to 200 pieces per size with immediate warehouse dispatch in 3 to 5 business days. Custom CNC components or non-standard tube wall dimensions manufactured to customer STEP/DWG drawings typically require an MOQ of 500 units with 2 to 3 weeks tooling and production lead time.
How does acoustic resonance differ between titanium and stainless steel exhaust systems?
Titanium has a lower density (4.51 g/cm³ vs. 7.93 g/cm³) and thinner wall profiles (1.0mm vs. 1.5mm), which shifts the natural acoustic resonant frequencies of the exhaust piping higher. This produces the characteristic higher-pitched, exotic engine howl prized in supercars and track vehicles, while substantially eliminating the lower-frequency cabin drone common to heavier stainless steel systems.
Ready to Optimize Your Titanium Exhaust Supply Chain?
Whether you require standard Grade 1 thin-wall tubing, CNC-machined pie cuts, or high-temp Grade 5 exhaust manifold studs, Navzo delivers verified Baoji mill pricing with an average 1-hour engineering response time.