High-Performance Titanium Valve Caps & Fastener Solutions
Manufactured using aerospace-grade Ti-6Al-4V bar stock. Featuring Swiss CNC precision threading, internal chemical-resistant O-rings, and custom anti-corrosion surface treatments.
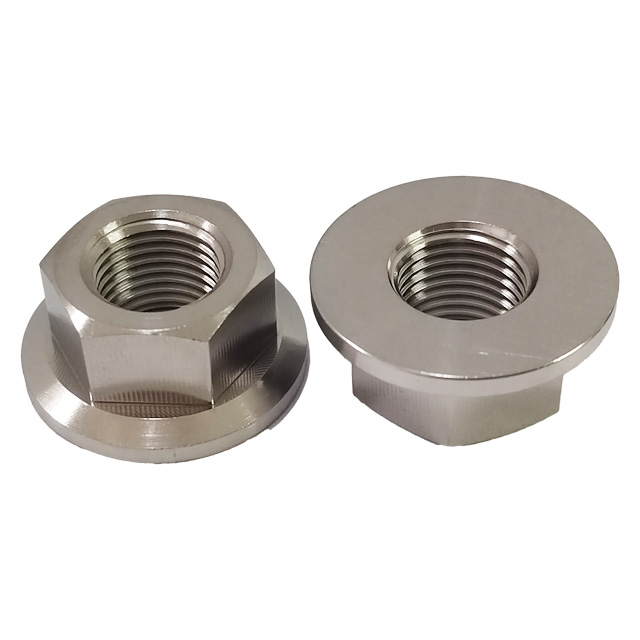
GR5 Titanium Nuts M12*1.5 High Strength Hex Flange Full Thread Nuts Factory Price Right Hand Fastener Nuts
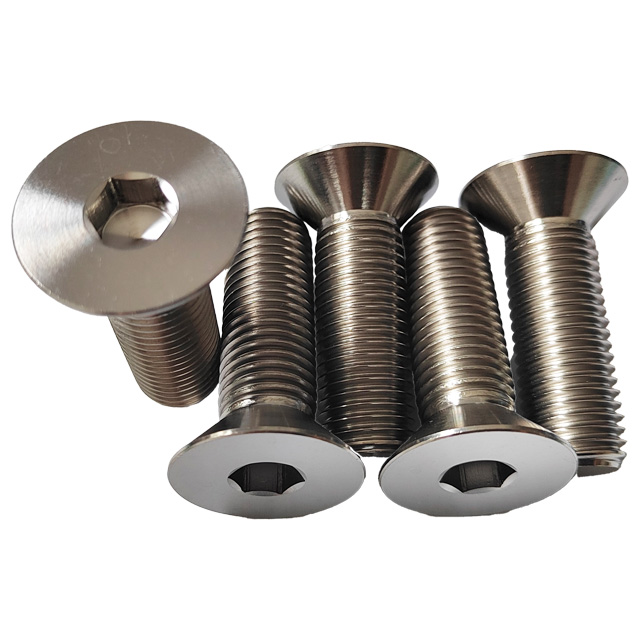
GR5 Titanium Bolts M10*20mm Factory Price Countersunk Head Hex Socket Bolts High Quality Round Head Inner Hex Screws
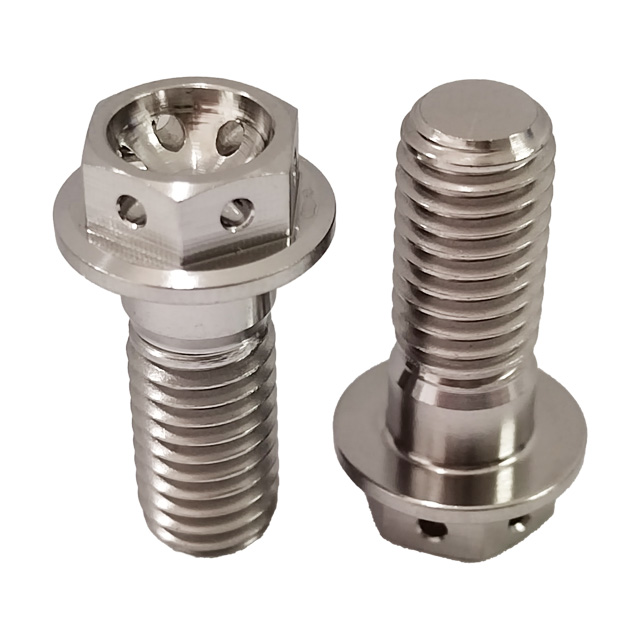
GR5 Titanium Bolts M8*20mm Factory Price Hex Flange Head Drilled Bolts High Quality Flange Head Slotted Screws
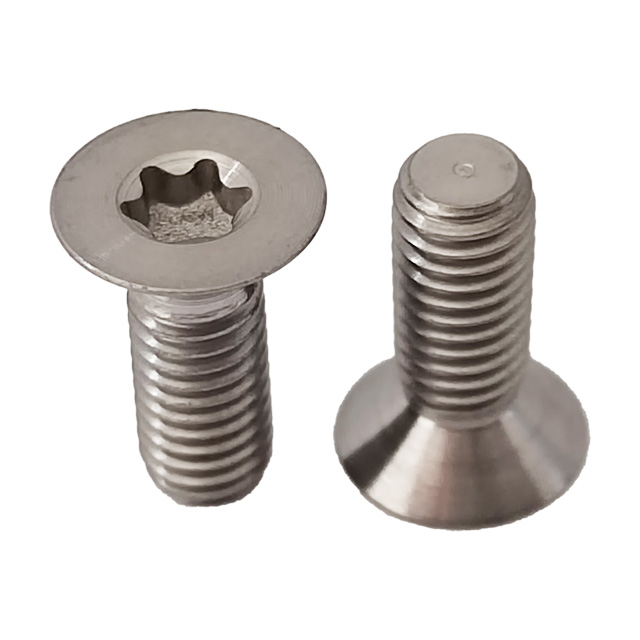
GR5 Titanium Bolts M5*13mm Lightweight Countersunk Head Inner Torx Bolts Factory Price Flat Head Inner Plum Screws
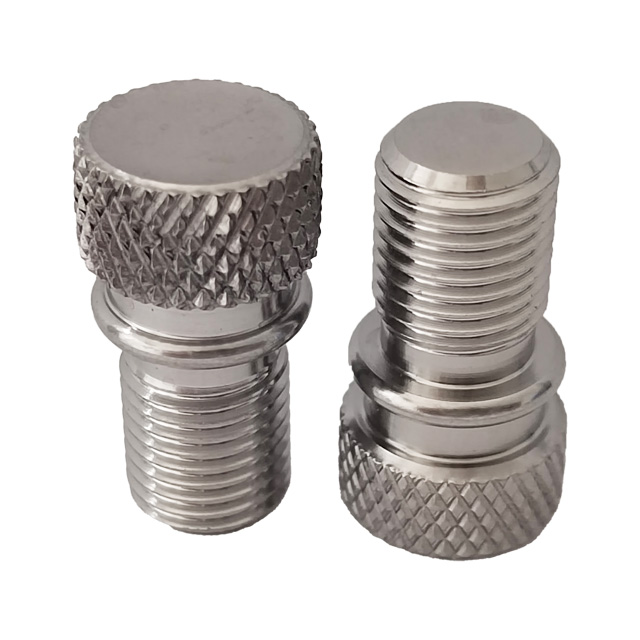
GR5 Titanium Bolts M9*1.0*12mm Hot Sale Cylindrical Head Knurled Bolts Factory Price Hand-Tightening Screws
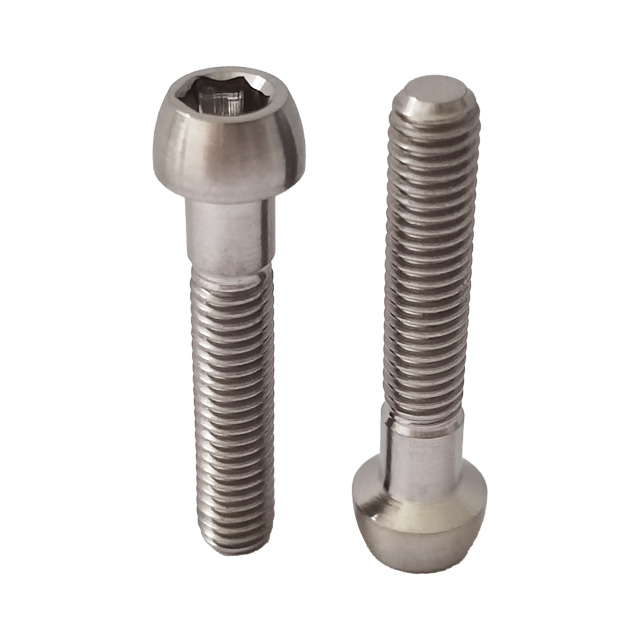
GR5 Titanium Bolts M6*31mm High Strength Tapered Head Hex Socket Bolts Factory Price Conical Head Inner Hex Screws
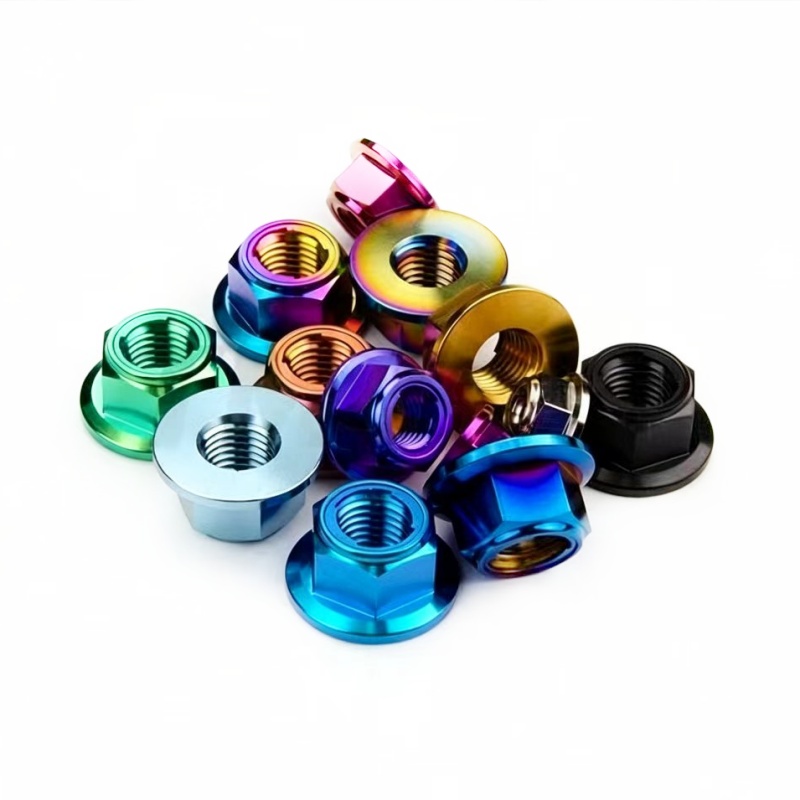
GR5 Titanium Lock Anti Loosening Nut Bicycle Motorcycle Car Locked Tightly Titanium NUTSM6 M8 M10 PVD Finished
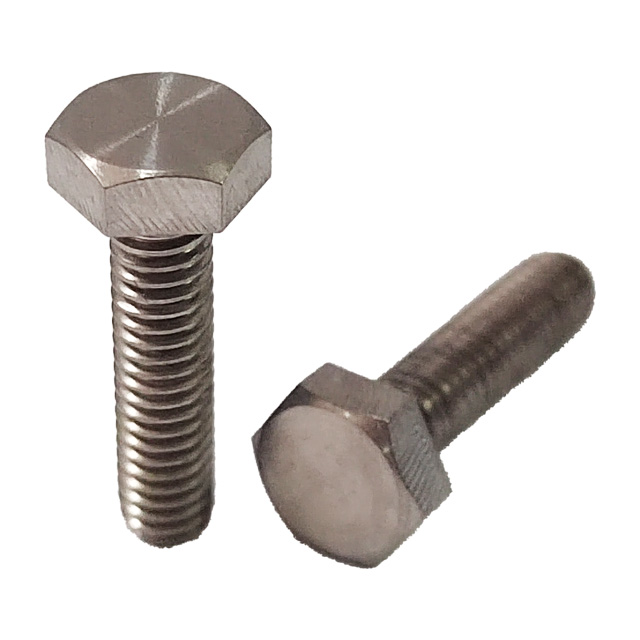
GR5 Titanium Bolts M4*15mm Factory Price Hexagon Head Full Thread Bolts High Strength Flat Head Screws
Engineering Superiority: Custom OEM Titanium Valve Caps Architecture
A rigorous metallurgical and mechanical evaluation of Ti-6Al-4V alloy applications in pneumatic sealing, galvanic barrier mitigation, and unsprung rotational mass reduction.
1. The Engineering Rationale: Why Titanium Outperforms Brass, Aluminum, and Polymer
In high-velocity automotive, track racing, and high-end cycling environments, tire valve caps serve far more than an ornamental function. They are the secondary defense perimeter against pneumatic pressure loss, contamination intrusion, and core corrosion. Traditional plastic caps are brittle, degraded by UV exposure, and fail to retain hermetic integrity under extreme centrifugal loading. Conventional aluminum caps frequently undergo severe galvanic corrosion when threaded onto brass or alloy valve stems, causing chemical bonding (galling/fusing) that shears valve stems during removal.
Navzo utilizes aerospace-certified Grade 5 Titanium (Ti-6Al-4V) bar stock. With an extraordinary strength-to-weight ratio, titanium provides absolute resistance against road deicing salts (calcium chloride, sodium chloride), brake dust caustic compounds, and UV radiation. Moreover, its passivated stable titanium dioxide (TiO₂) oxide layer eliminates the typical galvanic bonding mechanisms common to soft aluminum caps, guaranteeing seamless serviceability across multi-year duty cycles.
| Engineering Material | Density (g/cm³) | Tensile Strength (MPa) | Yield Strength (MPa) | ASTM B117 Salt Fog Resistance | Galvanic Fusing Tendency |
|---|---|---|---|---|---|
| Grade 5 Titanium (Ti-6Al-4V) | 4.43 | 895 – 1,000 | 828 | > 1,000 hrs (Zero Pitting) | Extremely Low (With Passivated TiO₂) |
| Commercially Pure Ti (Grade 2) | 4.51 | 345 – 450 | 275 | > 1,000 hrs (Zero Pitting) | Extremely Low |
| 6061-T6 Aluminum Alloy | 2.70 | 310 | 276 | < 96 hrs (White Rust / Pitting) | High (Severe Chemical Galling with Brass) |
| C36000 Free-Cutting Brass | 8.50 | 380 | 310 | 168 hrs (Verdigris Oxidation) | Moderate |
| 304 Stainless Steel (A2-70) | 7.93 | 700 | 450 | 240 hrs (Pitting at thread roots) | Moderate-Low (Excessive Unsprung Mass) |
2. Multi-Axis CNC Thread Precision & Dual-O-Ring Sealing Technology
A frequent flaw in mass-market valve caps is thread runout. Inferior roll-threading or loose CNC tolerances produce pitch diameter deviations, leading to cross-threading, vibration-induced back-off, or failure to compress the sealing elastomer properly. Navzo machines every custom titanium valve cap from solid solid bar using 5-axis Swiss-type precision lathes, maintaining internal thread tolerances within ISO 6H / 4H Class specifications.
- Schrader Thread Geometry (ISO 4570 / 8V1): Machined with 0.32-32 UNEF thread profiles. Engineered with internal relief grooves to seat flush against automotive TPMS (Tire Pressure Monitoring System) valve neck shoulders without interfering with stem electronics.
- Presta Valve Profiles (DIN 7756 / 5V2): Engineered for cycling rim profiles. Internal thread length is calibrated to isolate the brass locknut of Presta cores, preventing inadvertent unthreading during rapid top-offs.
- Chemical-Resistant Viton (FKM) / Silicone O-Rings: Every Navzo titanium cap incorporates a precision-recessed internal Viton (FKM) elastomeric ring. This forms an airtight secondary hermetic barrier that withstands continuous operating pressures of over 200 PSI and thermal thresholds from -40°C to +200°C.
- Dynamic Centrifugal Mass Balance: At 250 km/h, eccentric valve cap weight causes rotational imbalance and stem deflection. Titanium reduces component weight by 45% compared to steel/brass, neutralizing centrifugal stem bending moments.
3. Surface Modification: Vacuum PVD vs. Electrochemical Anodizing
Surface treatment on titanium is not merely cosmetic; it dictates wear resistance, surface harness, and long-term colorfastness against aggressive automotive cleaning chemicals, brake fluids, and environmental grit:
- PVD (Physical Vapor Deposition) Vacuum Sputtering: Titanium nitride (TiN - Gold), Titanium Carbonitride (TiCN - Bronze/Rose Gold), and Diamond-Like Carbon (DLC - Obsidian Black). Delivers a Vickers hardness of 2,200–3,000 HV, offering ultimate scratch resistance against gravel impact.
- Micro-Voltage Controlled Electrochemical Anodizing: Color is created by precise nanometer-scale manipulation of the transparent TiO₂ interference layer using controlled DC voltage (15V to 110V). Yields vivid electric blue, purple, magenta, and emerald green finishes without organic pigments or fading risks.
- Thermal Torch Gradient ("Burnt Blue"): Precision induction heating generates a flowing transition from gold to cobalt blue, honoring the traditional aesthetics celebrated in high-end JDM motorsport and titanium exhaust fabrication.
2025–2030 Global Procurement & Development Trends
How Tier-1 automotive brands, performance aftermarket suppliers, and cycling OEMs are structuring their titanium component supply chains.
Rapid Prototyping to High-Mix Low-Volume Production
Procurement teams are shifting away from monolithic multi-thousand-piece MOQ requirements. Modern ERP and CAD-to-CAM automation enable flexible production batches (300–1,000 units), allowing brands to test customized laser knurling patterns and bespoke limited-edition finishes without balance-sheet inventory liabilities.
Smart Sensor & TPMS Valve Stem Harmonization
As smart tire monitoring systems and internal rim Bluetooth transmitters become mandatory worldwide, valve caps must comply with precise thread clearances. Future designs incorporate anti-static grounding continuity and non-shielding cap architectures that do not interfere with high-frequency BLE 2.4 GHz tire telemetry transmission.
Integrated Anti-Theft & Multi-Functional Tool Geometry
High-value titanium components represent attractive targets for retail theft. Contemporary procurement trends demand stealth anti-theft designs featuring integrated tamper-resistant hex flats, security star keys, or built-in core valve removal wrenches integrated directly into the knurled cap crown.
Why Tier-1 Engineers Partner with Navzo Precision Titanium
Operating from China's legendary "Titanium Valley" in Baoji since 2011, Navzo combines upstream metallurgical raw material access with downstream multi-axis CNC execution.
Baoji Ingot Sourcing
Direct supply agreements with primary Baoji titanium sponge and bar mills provide 100% material lot traceability, complete with EN 10204 3.1 Mill Test Certificates for every batch.
Integrated CNC Fleet
Equipped with high-precision CNC turning, 5-axis Swiss-type automated lathes, multi-station cold heading machines, and precision thread-rolling facilities under one unified roof.
In-House Metrology
Thread optical profile projectors, automated coordinate measuring machines (CMM), surface roughness profilometers, and ASTM B117 salt fog testing chambers guarantee compliance.
Sub-Hour Engineering RFQ
Our bilingual mechanical engineering team reviews client 2D (PDF/DWG) and 3D (STEP/IGES) CAD files with an average RFQ turnaround time under 60 minutes during standard trade hours.
Navzo Custom OEM / ODM Engineering Execution Process
Reviewing thread fit tolerances, O-ring groove depth, knurling depth, and laser logo specs.
Spectrometry confirmation of chemical composition for Grade 5 (Ti-6Al-4V) bar stock prior to cutting.
Simultaneous turning, knurling, chamfering, internal single-point thread tapping, and parting off.
Automated ultrasonic cleaning followed by anodizing, burnt blue thermal oxidation, or vacuum PVD.
100% thread Go/No-Go plug gauge inspection, O-ring insertion, blister cards or private label boxes.
Frequently Asked Questions for B2B Importers & Engineers
Clear, definitive answers addressing thread galling, material authenticity, coating life, and export logistics.
Will titanium valve caps fuse or seize onto aluminum or brass valve stems?
Unlike cheap aluminum caps that form galvanic aluminum-brass galvanic batteries leading to solid oxide fusion, titanium has a passivated TiO₂ layer with poor galvanic conductivity. While titanium-to-aluminum galling risk is inherently low, Navzo machines high thread clearances (6H) and equips internal elastomeric stops to eliminate binding. For winter climates with road salt, applying a micro-film of anti-seize or synthetic fluoropolymer grease ensures effortless removal forever.
How does Navzo verify Grade 5 (Ti-6Al-4V) authenticity versus cheap scrap titanium?
Every raw material billet undergoes spectral chemical analysis and mechanical pull testing. Grade 5 titanium must rigorously contain 5.5%–6.75% Aluminum and 3.5%–4.5% Vanadium with iron content capped below 0.40%. Certified Mill Test Reports (MTR) according to EN 10204 3.1 accompany every international delivery, protecting buyers from commercially pure (Grade 2) substitution.
What is your standard OEM minimum order quantity (MOQ) and sample lead time?
For catalog sizes (Schrader 8V1 and Presta 5V2 in standard knurl and anodized finishes), our MOQ is 100 to 200 sets. For custom CNC drawings with bespoke outer knurling profiles, brand laser engraving, or PVD rainbow/DLC coatings, production runs start at 500 sets. Precision CNC prototype samples can typically be fabricated and dispatched within 3 to 7 business days.
Can you provide private label packaging and custom laser etching?
Yes. Over 70% of our export clients utilize our comprehensive OEM packaging support. We offer high-definition fiber laser engraving of brand logos or torque indicators (repeatable down to 0.1 mm precision), EVA foam custom presentation boxes, printed blister packaging, barcoded retail hang-cards, and laser-etched orientation dots.
Are Navzo titanium valve caps compatible with high-pressure Tubeless cycling systems?
Yes. Our Presta valve caps are specifically tailored for modern high-pressure road tubeless (up to 120 PSI) and low-pressure MTB tubeless systems. The internal Viton seal prevents sealant spray-out and stops coagulated latex liquid from fouling the valve core threads, ensuring flawless depressurization during service.
What quality inspection certifications and dimensional guarantees are supplied?
Quality control operates under ISO 9001 quality management guidelines. Prior to packaging, thread tolerances are verified using Class 6H Go / No-Go gauges. We perform 100% visual inspection for micro-burrs, knurl crispness, and uniform color shade matching under standard D65 illuminants. Full CMM inspection reports are available on request.